Category: Technical Guides

  • RTO Outlet VOC Spikes: A Root-Cause Isolation Workflow for Plant Teams

    RTO Outlet VOC Spikes: A Root-Cause Isolation Workflow for Plant Teams

    RTO Outlet VOC Spikes: A Root-Cause Isolation Workflow for Plant Teams

    When an RTO outlet VOC result rises unexpectedly, the fastest response is rarely to change a setpoint. An outlet concentration can move because the process load changed, the sample no longer represents the stream, a valve or purge sequence altered flow, the thermal profile became unstable, or the analyzer and historian are not aligned in time. Treating every spike as an oxidizer failure can create unnecessary risk and obscure the evidence needed for a durable fix.

    This guide provides a practical root-cause isolation sequence for operations, maintenance, EHS, and engineering teams. It is a troubleshooting framework, not a substitute for the approved design basis, permit, test method, lockout procedure, or a competent emissions-testing organization. Use the limits and valid-run rules applicable to the installed system.
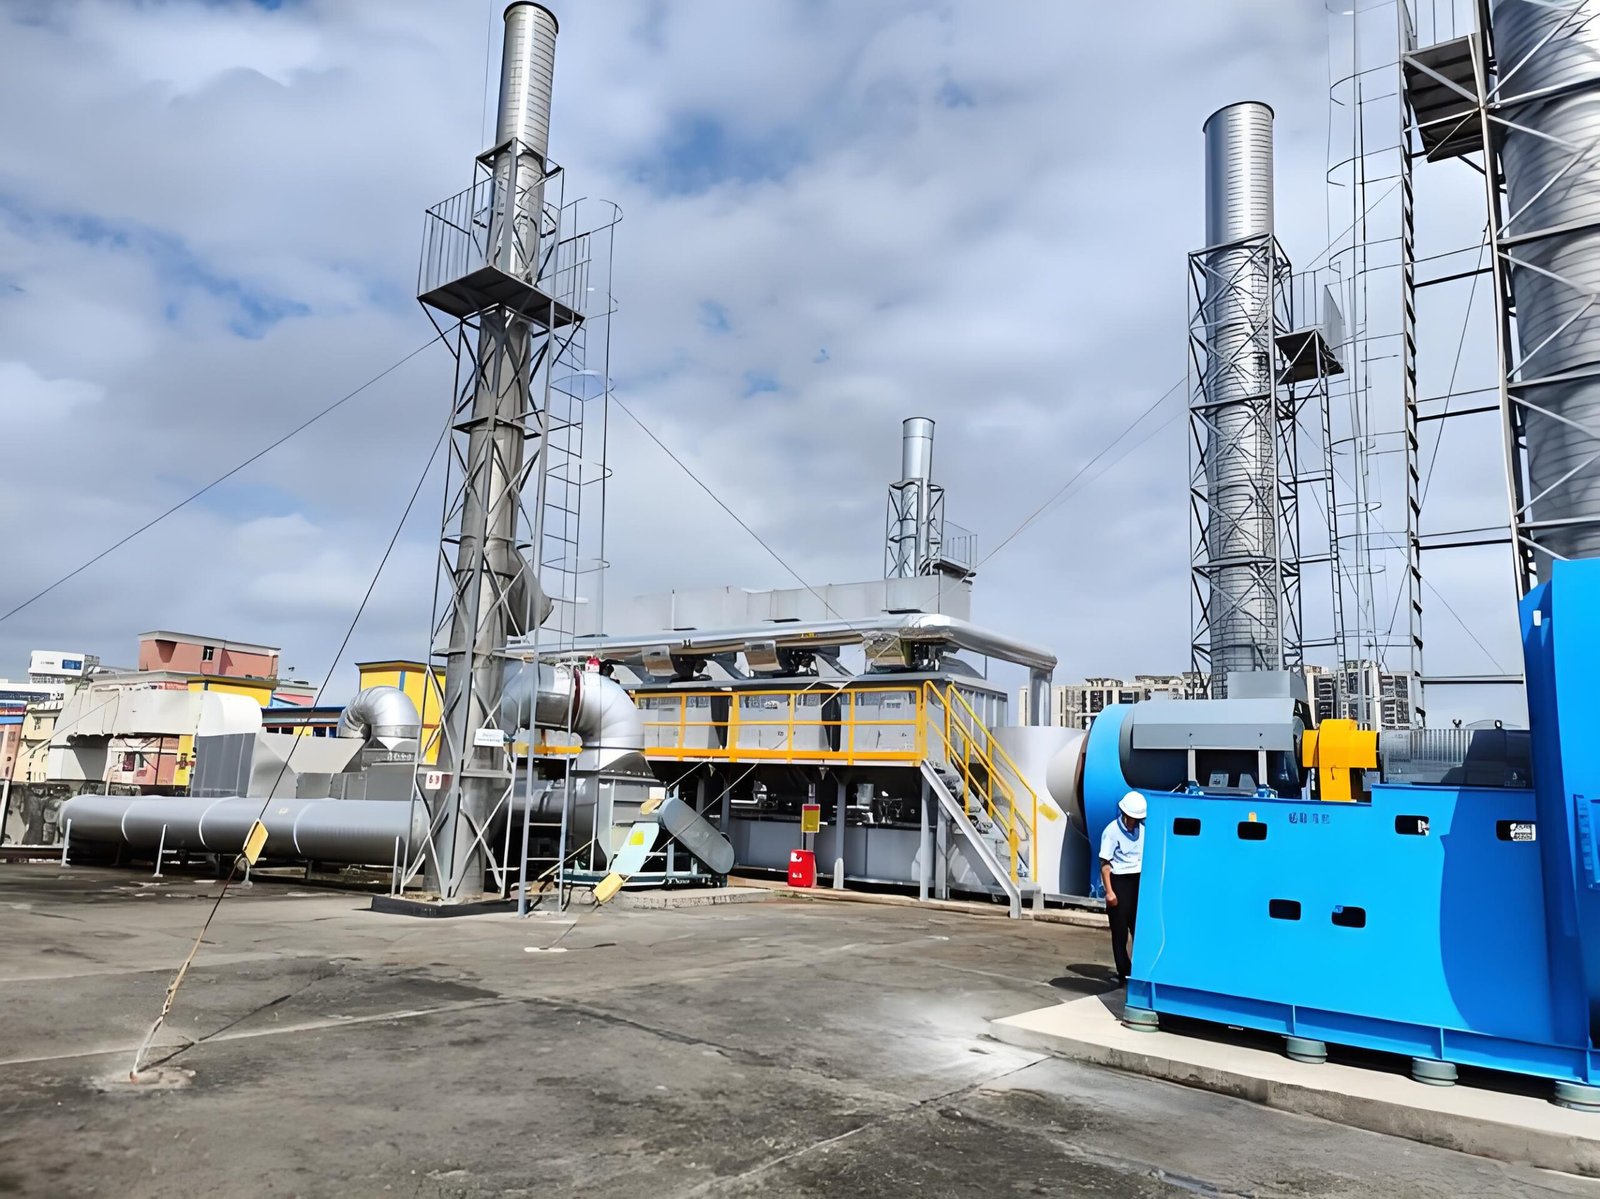
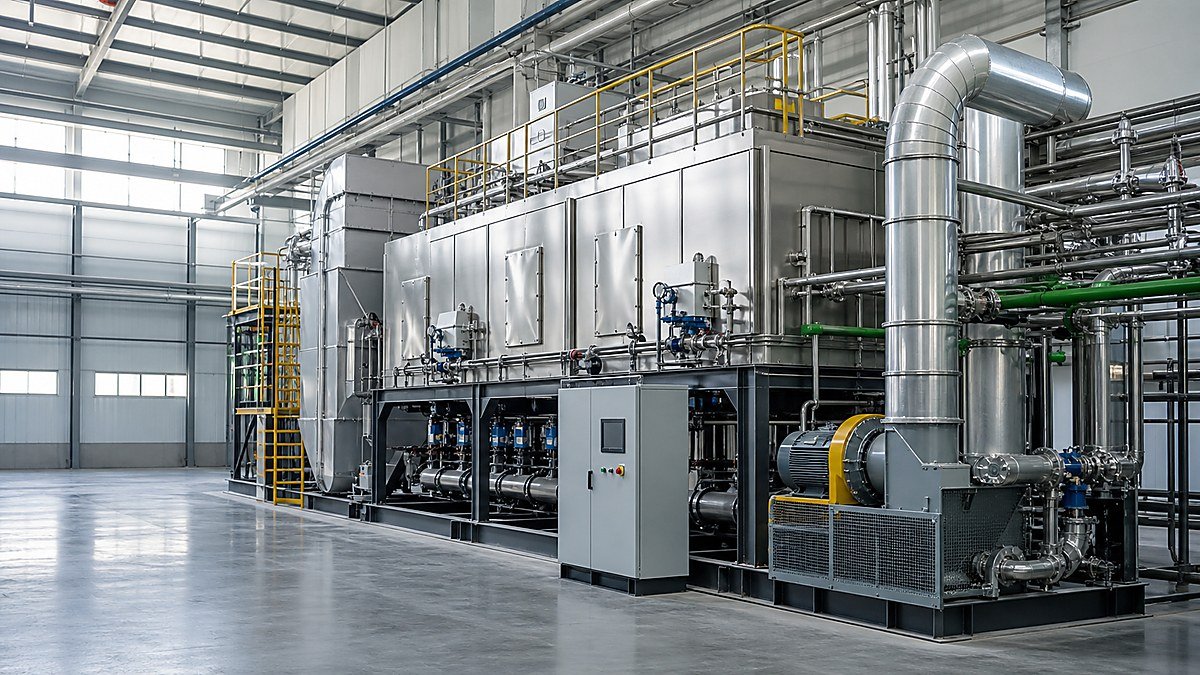
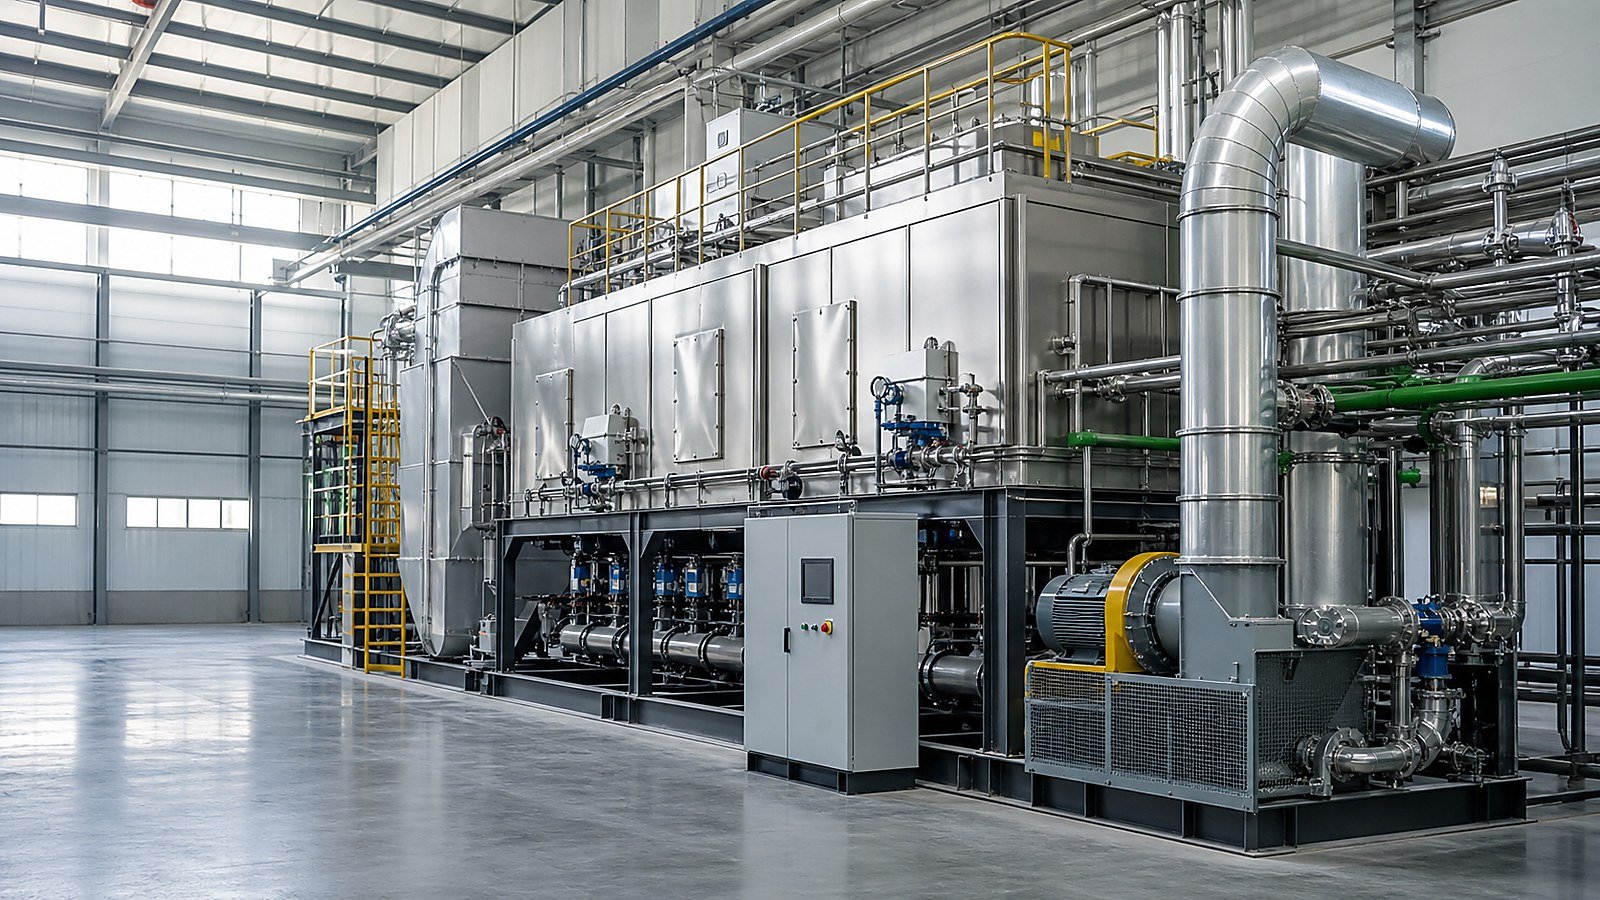
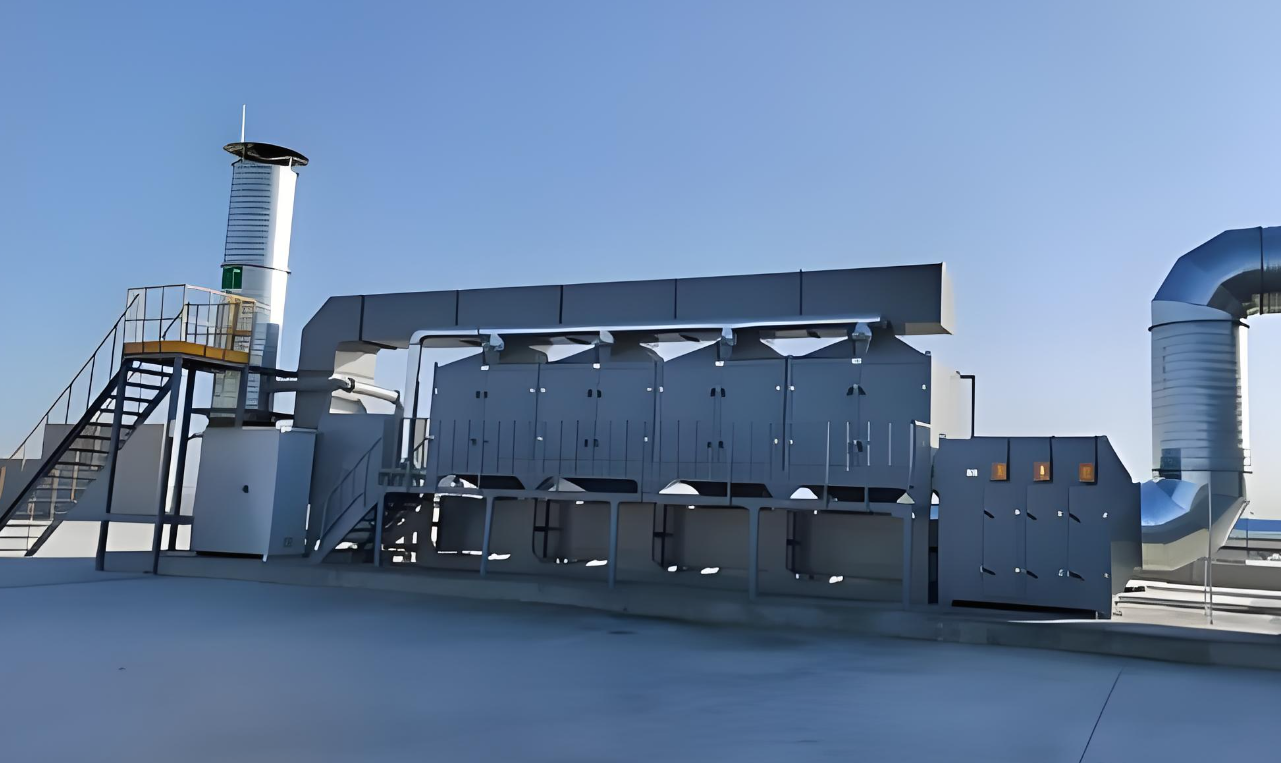
    RTO equipment and combustion-air ductwork reviewed during an outlet VOC root-cause investigation

    1. Confirm that the spike is real and comparable

    Start by preserving the original record: sample ID, analyzer file, historian trend, unit, reference condition, location, operator notes, and exact timestamps. Do not average away an unusual point before understanding it.

    Ask four comparison questions:

    • Is the result from the same outlet location, method, basis, and averaging period as the prior result?
    • Were the sample train, probe, filters, conditioning, and leak checks acceptable?
    • Do the PLC trend, portable instrument, and laboratory result refer to the same time window?
    • Did the sample coincide with startup, a recipe change, a damper movement, purge, alarm, or manual intervention?

    If the measurement chain is not comparable, classify the event as a data-quality investigation first. That does not prove the process was healthy; it tells the team what must be re-measured.

    2. Reconstruct the process load at the RTO inlet

    The RTO can only treat the stream that actually reaches its inlet. Reconstruct source status and loading for the spike window using batch records, solvent or coating usage, production rate, exhaust fan status, and any dilution or make-up air.

    Evidence to compareWhy it mattersImmediate check
    Source on/off and damper positionA new or missing source changes concentration and flowCompare PLC state with operator log
    Recipe, solvent, coating, or resin changeVOC species and concentration can shift without an RTO changeMatch batch record to sample time
    Production rate and simultaneityPeak loading may exceed the assumed operating casePlot source rates and total flow
    Dilution or make-up airIt can lower concentration while increasing volumetric flowCheck fan and damper commands
    Moisture, mist, dust, or acid gas carryoverPretreatment or condensation issues can bias sampling and foul componentsReview upstream separator and drain status

    Avoid inferring mass loading from concentration alone. Flow, temperature, pressure, moisture, and the reference basis must be reviewed together.
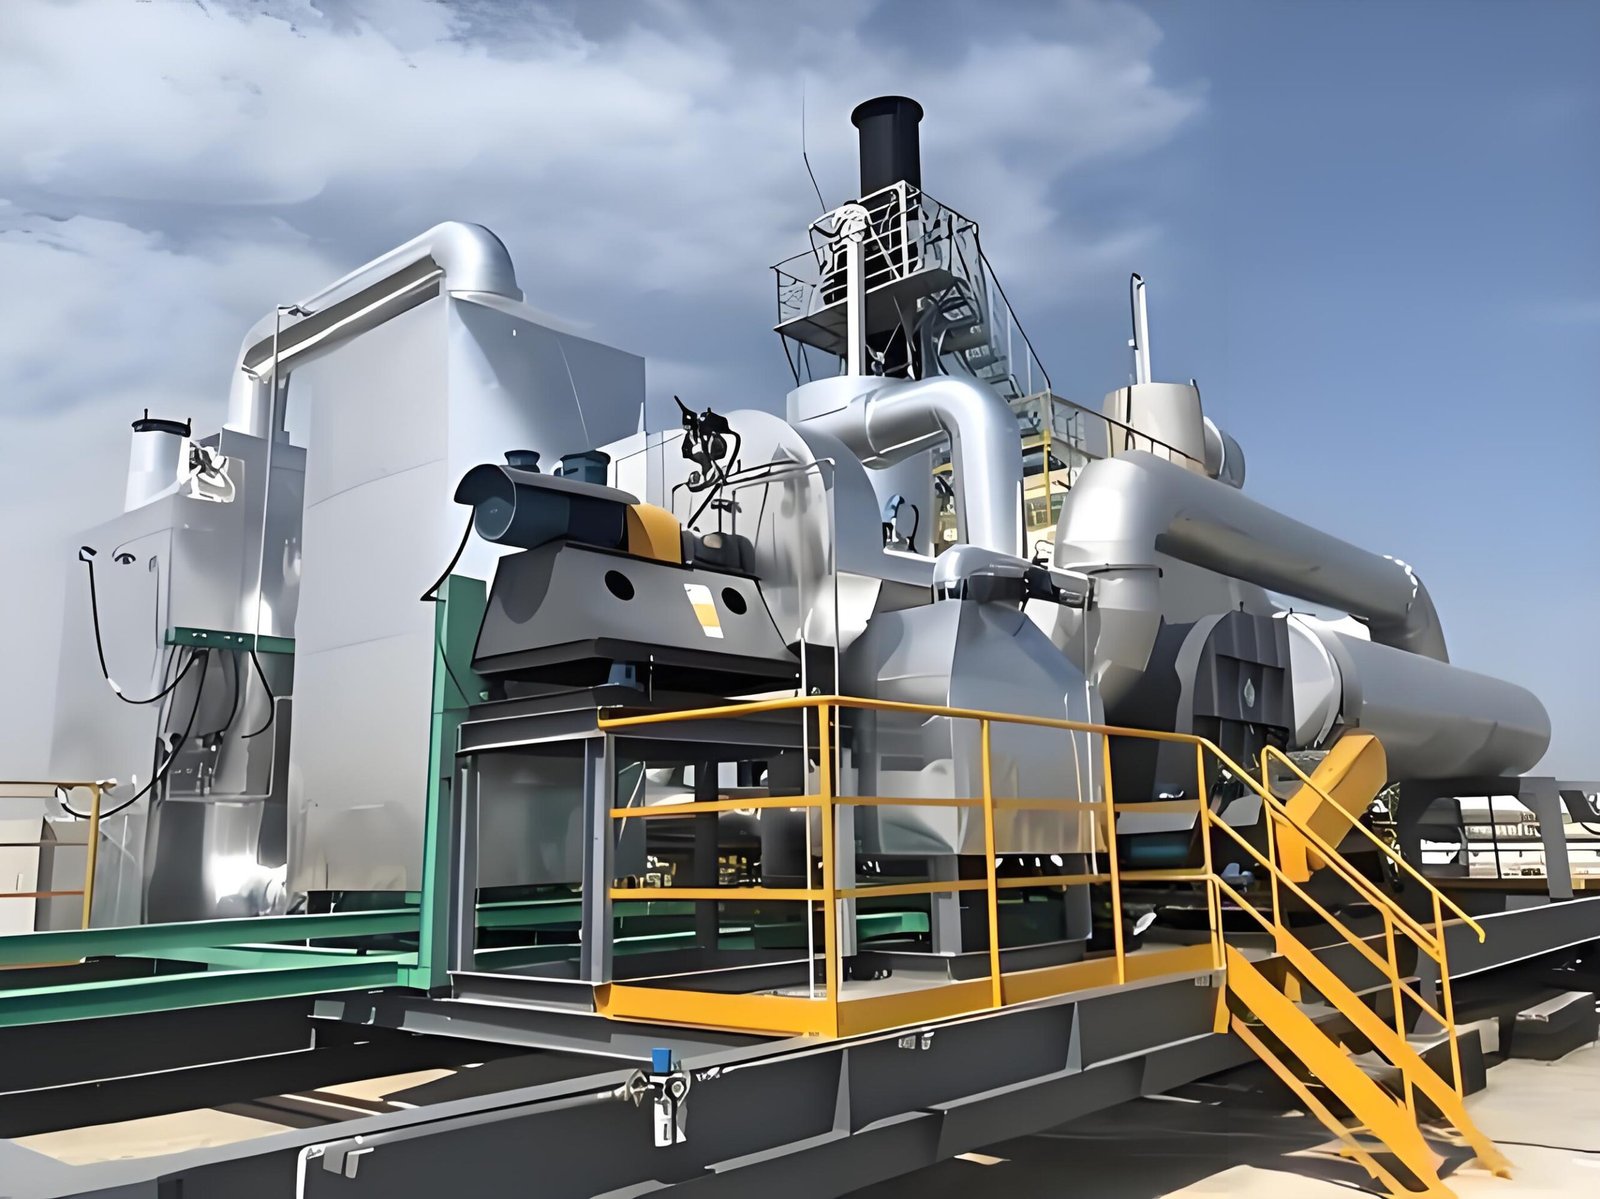
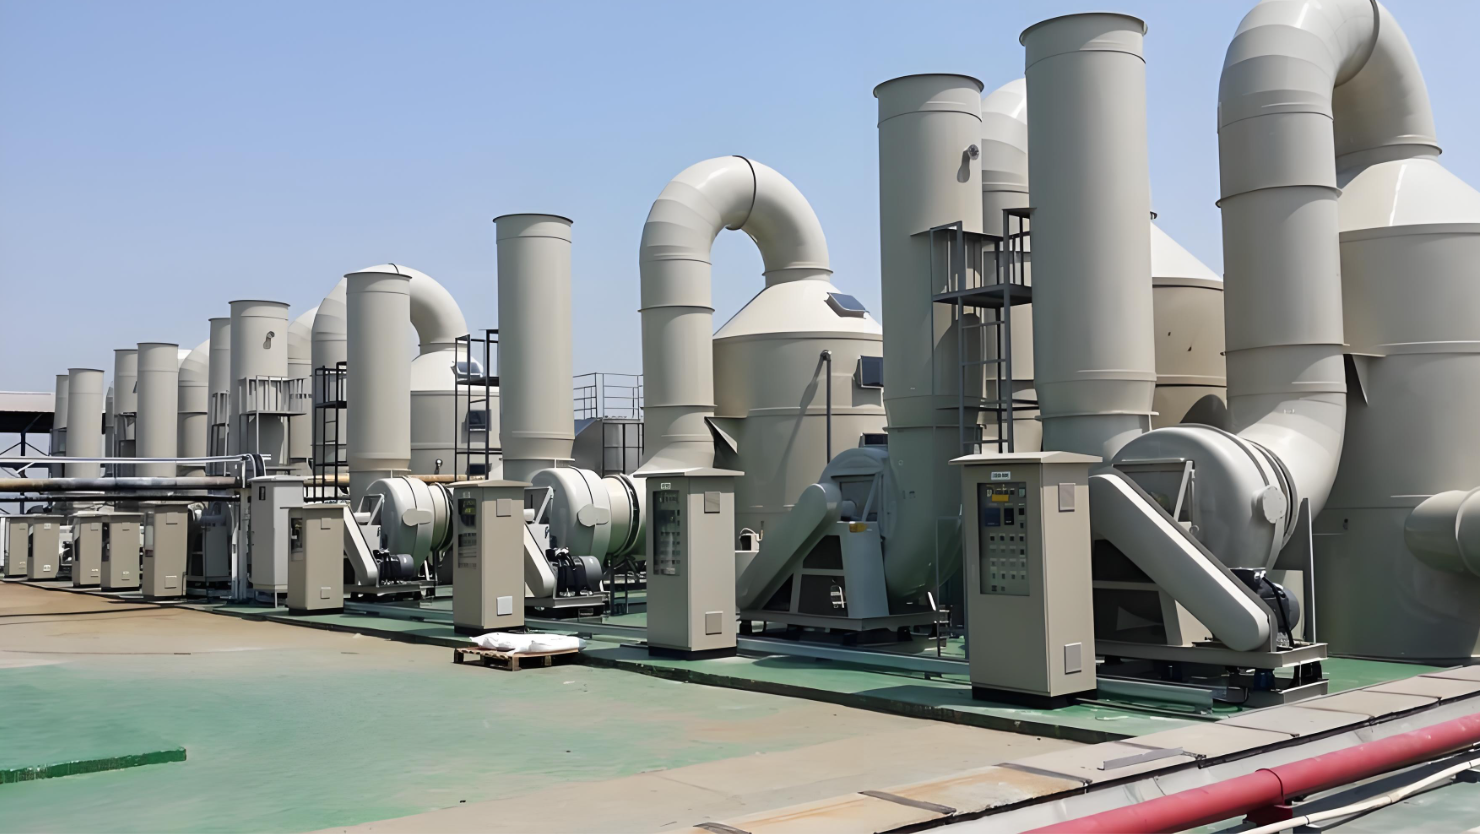
    RTO burner-air ducting and service access used to check flow and thermal behavior

    3. Check flow distribution and fan conditions

    Uneven flow can leave part of the ceramic bed under-used while another path is overloaded. Review fan speed, inlet and outlet pressure, damper feedback, purge flow, and any recent duct or filter work. A command that says “open” is not proof that the damper reached its intended position.

    Use a simple before/after comparison with the same operating case. Look for a step change after maintenance, a gradually increasing pressure drop, hunting fan control, or a mismatch between redundant transmitters. Verify impulse lines and transmitter ranges before concluding that the process airflow changed.

    For a site investigation, record the measurement point, units, reference conditions, and whether the reading is indicated, calculated, or independently checked. A trend without that metadata is difficult to defend.

    4. Verify thermal state and cycle behavior

    Review chamber temperatures, bed temperatures where available, cycle timing, burner demand, fuel status, and high-temperature or low-temperature alarms. A single high temperature does not prove complete treatment, and a normal outlet temperature does not rule out short-circuiting or a measurement problem.

    Check whether the spike aligns with a cycle transition, purge event, burner modulation, or a period of low VOC loading that required support fuel. Compare the actual sequence with the approved control narrative. Record any temporary override, forced output, inhibited alarm, or manual mode and its authorization.

    Do not change temperature or cycle settings solely to chase one result. First determine whether the event is repeatable under a controlled, safe operating case.

    5. Isolate valves, purge, and bypass paths

    Valve leakage, incomplete seating, wrong sequence, and purge timing can all create an outlet concentration increase, but they leave different evidence. Compare command, feedback, travel time, actuator air, limit-switch status, and pressure response for each relevant valve.

    Check for:

    1. a feedback signal that remains unchanged while the command moves;
    2. a travel-time increase or repeated position timeout;
    3. a pressure or temperature response inconsistent with the intended flow path;
    4. a purge or bypass state that overlaps the sample window; and
    5. maintenance work, seal replacement, or calibration immediately before the event.

    Follow the site’s isolation and permit rules before any physical inspection. A software trend can identify a suspect path; it cannot authorize opening equipment.

    6. Recheck sampling and analyzer integrity

    If equipment trends look normal, return to the measurement chain. Confirm sample-port location, probe orientation, heated-line temperature, condensate management, filter condition, calibration gas, zero/span checks, response time, and data logging. Review whether the analyte or concentration range is suitable for the instrument.

    For laboratory work, preserve chain of custody and retain field blanks, duplicates, raw chromatograms or analyzer files where applicable, and any method deviations. A repeat sample should deliberately reproduce the same operating case while documenting what changed.

    7. Decide the next test from the evidence

    Use a decision log rather than a list of guesses. Each hypothesis should have a predicted signature and one safe check:

    HypothesisExpected signatureSafe next check
    Process loading changedInlet flow/concentration and source records move togetherRepeat under a defined production case
    Flow distribution issueFan, pressure, damper, or purge trend is abnormalVerify feedback and compare paths
    Thermal/cycle instabilityBed or chamber trend changes with cycle eventsReview sequence and authorized alarm history
    Valve or bypass pathCommand/feedback/pressure mismatchFunctional test under permit
    Sampling/analyzer issueEquipment trends stable; sample quality flags presentQA check and controlled resample

    Stop and escalate when the evidence points to an unsafe condition, an inhibited safety function, an uncontrolled bypass, or an out-of-design operating case. The correct outcome may be a repeat test, maintenance action, process restriction, or design-basis review—not an improvised setpoint change.

    FAQ

    Does an outlet VOC spike always mean the RTO destruction efficiency fell?

    No. It may be a real treatment change, a higher or different inlet load, flow short-circuiting, or a sampling and analyzer problem. Compare the full operating case and measurement chain.

    What should operators capture first?

    Preserve the exact sample and trend timestamps, source status, production recipe, flow/pressure, temperatures, cycle state, alarms, valve commands and feedback, and any manual intervention.

    Can I use a generic temperature threshold to clear the event?

    No. Use the installed system’s approved design basis, control narrative, permit, and test method. A generic threshold can be misleading or unsafe.

    When is a repeat sample justified?

    When the operating case can be reproduced safely and the initial sample has a quality concern, an unexplained mismatch, or a documented deviation. Define what will be held constant and what will be checked differently.

    Can SERNO help with a troubleshooting review?

    SERNO can organize source data, operating trends, sample records, and a hypothesis-to-check matrix for a site-specific engineering discussion. Final safety, compliance, and operating decisions remain with qualified site personnel.

    Conclusion

    An RTO outlet VOC spike deserves a traceable investigation, not a reflexive setpoint change. Confirm the measurement, reconstruct inlet loading, check flow and thermal behavior, isolate valves and bypasses, then choose a controlled repeat test or corrective action from the evidence. This sequence helps plant teams protect safety, reduce downtime, and produce a reviewable record for engineering and EHS.

    For a site-specific review, SERNO can help structure the data request and root-cause matrix around your actual sources, RTO configuration, and approved operating documents.
  • RTO Performance Verification: What to Prepare Before a Buyer Acceptance Test

    RTO Performance Verification: What to Prepare Before a Buyer Acceptance Test

    RTO Performance Verification: What to Prepare Before a Buyer Acceptance Test

    An RTO performance verification is not simply a day when someone records outlet data. It is a controlled demonstration that the installed system can operate in an agreed process case and produce the evidence defined in the purchase or commissioning documents.

    The difficult work usually happens before the test: deciding which production sources run, defining stable conditions, checking instruments and sample locations, agreeing how missing data will be handled, and assigning each acceptance row to an owner. If those decisions remain implicit, a technically sound test can still produce an argument about whether the result is representative.

    This guide is an engineering preparation framework for buyers, operations, EHS, commissioning, and suppliers. It does not replace the contract, approved design basis, site procedures, or the competent test organization responsible for sampling and interpretation.

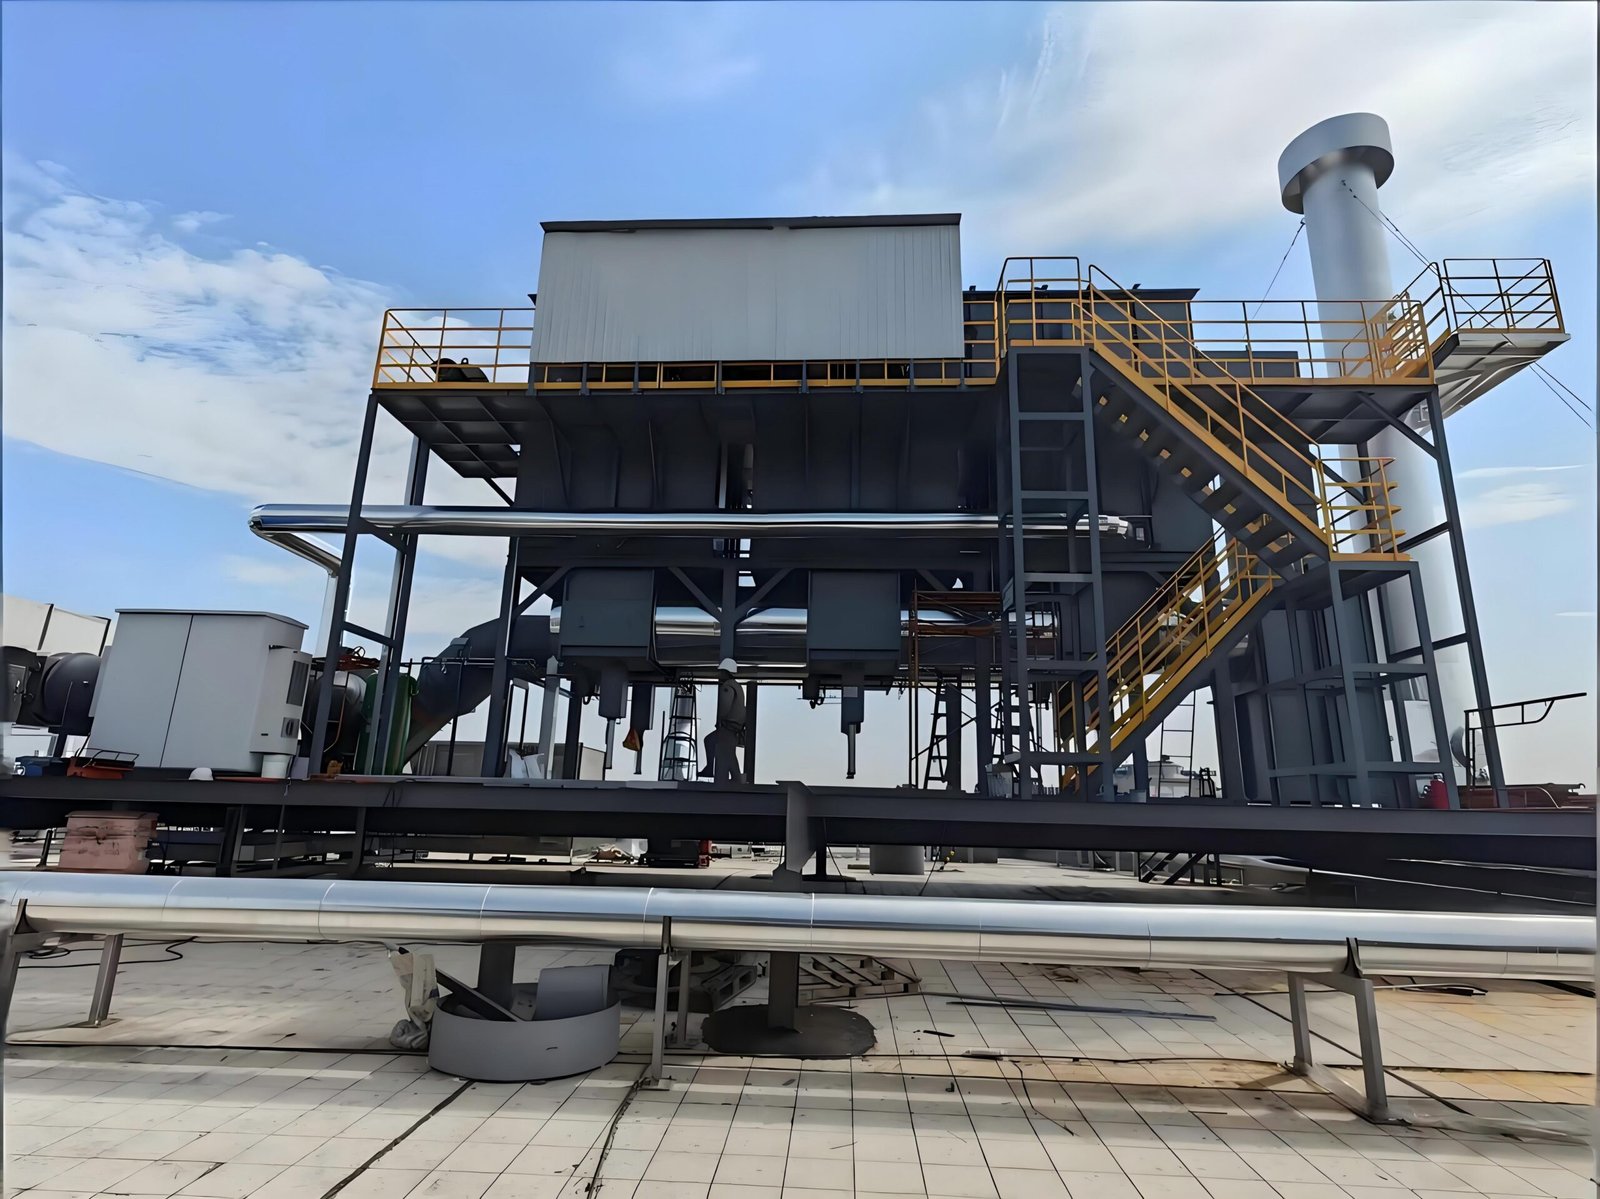
    Exterior RTO equipment used as context for preparing a performance verification test

    1. Define the approved test case before anyone takes a reading

    Write the test case in plain language and attach the current process and RTO documents. At minimum, identify the process sources connected to the system, the intended production state, the permitted operating mode, and the duration or number of valid runs required by the agreed test plan.

    Record the conditions that can materially change the result:

    • Which exhaust sources are operating, and are they expected to run simultaneously?
    • What production rate, material, solvent or coating recipe, and shift condition represent the approved case?
    • What airflow, temperature, pressure, VOC composition, and moisture range is expected at the RTO inlet?
    • Which bypasses, recirculation paths, dilution air, purge sequences, or startup states are excluded?
    • What happens if the process changes or a reading leaves the agreed range?

    A test case is useful only when operations can recognize it on the day. Use tags, historian trends, batch records, and operator sign-off to show that the stated case actually occurred.

    2. Turn the acceptance requirement into measurable rows

    Convert the contract or commissioning requirement into an acceptance matrix. Do not leave a phrase such as “meets performance” without a measurement definition, owner, and evidence source.

    Acceptance rowMeasurement definitionEvidence ownerPre-test check
    Destruction or outlet concentrationAn agreed analyte, method, location, averaging rule, and valid-run ruleTest organization and EHSConfirm sample port, method, and laboratory instructions
    RTO operating conditionTemperature, cycle state, pressure, flow, and relevant alarms within agreed bandsControls and operationsVerify tags, historian points, and time synchronization
    Pressure or fan dutyDefined measurement points and reference conditionMechanical/controls teamCheck transmitter calibration and impulse lines
    Process representativenessSource status, production rate, material, and batch evidenceOperationsPrepare batch record and operator log
    Data completenessRequired timestamps, units, run duration, and treatment of invalid dataTest leadDry-run the data sheet and backup process

    For each row, state whether it is a guaranteed value, a design reference, an observation, or a condition for a valid test. That distinction keeps an observation from being mistaken for a contractual conclusion.

    3. Check instruments, sampling points, and data quality

    Before the test, make an instrument list with tag, range, unit, calibration status, and data source. Confirm that the range is suitable for the expected operating window; a sensor can be in calibration and still be poorly suited to the value being measured.

    Sampling preparation deserves the same discipline. Verify that ports are accessible, safe, identified, and located where the agreed method expects them. Confirm probe clearance, conditioning requirements, utilities, and any blank or leak checks required by the test organization. Do not infer a valid result from an easy-to-reach port that does not represent the intended stream.

    Synchronize clocks across the PLC, historian, portable instruments, laboratory labels, and operator logs. A five-minute mismatch can make a process change appear unrelated to a sample. Define the master time reference and record any correction.

    Use a short pre-test data-quality check:

    1. Compare the control-system value with an independent portable or reference reading where practical.
    2. Confirm units and reference conditions, especially for flow, temperature, and concentration.
    3. Check for flat-lined, clipped, implausibly fast, or intermittently missing signals.
    4. Record calibration certificates or verification results in the test file.
    RTO duct and access platform illustrating instrument and sampling-point preparation

    4. Prepare the RTO and process sources for a stable run

    The equipment should be mechanically and operationally ready before the first valid run starts. Complete open punch-list items that could affect the test, review active alarms, and confirm the approved valve sequencing, burner state, fan configuration, and safety permissives. A performance test is not the right time to discover that a temporary override is still active.

    The process side is equally important. Confirm source routing, damper positions, production recipe, material feed, and expected solvent or VOC loading. If a source is unavailable, document the substitution and obtain the test lead’s decision on whether the run remains valid.

    Define a stabilization rule that operators can follow. It may use a sustained period of acceptable temperature, flow, pressure, source status, and alarm-free operation. The exact values should come from the approved design basis or test plan, not from a generic blog threshold.

    Keep an event log with exact timestamps for startup, stabilization, sample start/stop, recipe or flow changes, alarms, manual interventions, and shutdown. A clean event log often explains more than a single average.

    5. Coordinate emissions sampling and chain of custody

    When external sampling or laboratory analysis is involved, align the field team, plant, and supplier before the test date. Confirm who supplies equipment, who observes the method, who labels samples, and who receives the final data package.

    The sampling plan should state the analytes, locations, number of runs, duration, field blanks or duplicates where required, sample containers, preservation, transport, and reporting units. The plan must also explain what happens when a sample is invalid or a process event interrupts a run.

    Use a chain-of-custody record that connects sample ID to location, start/stop time, operating case, sampler, preservation, and laboratory receipt. Keep copies with the test report. These records support traceability; they do not by themselves prove compliance with a particular jurisdiction’s rule.

    6. Separate test observations from pass/fail conclusions

    During the test, capture facts first: the operating state, instrument values, sample IDs, alarms, changes, and deviations. The technical team can then compare those facts with the agreed acceptance matrix.

    Use a deviation log with four fields:

    • what happened and when;
    • which acceptance row or test assumption it affects;
    • whether the run is valid, invalid, or requires a technical decision;
    • who approved the disposition and what follow-up evidence is required.

    Avoid editing data to make a trend look cleaner. If a value is corrected, preserve the original, the reason, the method, and the person who approved the correction. If a result is outside the agreed band, report it and explain the operating context rather than labeling it a failure without review.

    7. Close the evidence loop after the test

    The acceptance package should be usable by someone who was not in the control room. Assemble the signed test plan, operating-case evidence, calibration and method records, raw data, calculations, sample and laboratory records, event/deviation log, photos of relevant setup, and the final acceptance matrix.

    Hold a short close-out with operations, maintenance, engineering, EHS, procurement, and the supplier. Identify open actions such as repeat testing, instrument repair, documentation correction, or a design-basis update. Assign an owner and due date for each action. Link the final record to the RTO equipment tags and future maintenance or spare-parts reviews.

    FAQ

    Is an RTO performance verification the same as a regulatory compliance test?

    Not necessarily. A buyer acceptance or commissioning test may use contract-defined conditions and methods, while a regulatory test follows the applicable permit or rule. Confirm the governing requirement and competent test organization for the site.

    What if production cannot reach the planned operating case?

    Document the actual source status, recipe, flow, loading, and duration. Ask the responsible test lead and contract owners whether the run is representative, needs qualification, or must be repeated. Do not silently substitute a different case.

    How much data should be retained?

    Retain the complete package defined by the contract, site document control, and test method: raw data, calculations, calibration evidence, sample records, event logs, and approved deviations. A summary without traceable source data is difficult to review.

    Can the PLC historian alone prove performance?

    Historian data is valuable for operating context, but some acceptance rows require independent verification, calibrated instruments, or laboratory analysis. Match each conclusion to the evidence type stated in the acceptance matrix.

    Can SERNO help prepare an acceptance matrix?

    SERNO can help organize the process-source data, RTO operating points, measurement questions, and evidence owners for a site-specific technical discussion. Final acceptance decisions remain with the contract parties and qualified site personnel.

    Conclusion

    RTO performance verification is strongest when the test case, measurement method, equipment state, and evidence package are agreed before the first sample. Define measurable acceptance rows, check instruments and sample points, stabilize the process, log every event, and separate observations from conclusions. That preparation gives buyers a reviewable record and gives plant teams a clear path for any repeat or corrective action.

    For an upcoming RTO acceptance test, SERNO can review the available design basis, source data, operating scenarios, and draft acceptance matrix for a focused engineering discussion. Use the actual installation documents and qualified site procedures for final operating, safety, and compliance decisions.

  • RTO Critical Spare Parts: Build a Preventive-Maintenance Strategy Before an Outage

    RTO Critical Spare Parts: Build a Preventive-Maintenance Strategy Before an Outage

    RTO Critical Spare Parts: Build a Preventive-Maintenance Strategy Before an Outage

    Preventive maintenance is not complete when a work order is scheduled. For a regenerative thermal oxidizer (RTO), the team also needs a defensible answer to a practical question: if a component fails during the next operating period, can the plant restore the approved operating condition with the parts, information, and support it actually has?

    That answer is rarely found in a single bill of materials. RTOs combine gas-path equipment, valves, actuators, burners, instruments, fans, refractory or ceramic media, controls, and safety devices. The consequence of losing one item depends on the installed configuration, the process sources connected to it, the failure mode, and the time required to verify a repair. A low-cost seal can be more urgent than a higher-value assembly if it is unique, exposed to the process, or difficult to source.

    This guide presents a practical spare-parts strategy for an installed RTO. It does not prescribe a universal stock quantity or replace OEM instructions, site safety procedures, approved parts lists, or a qualified engineering review.

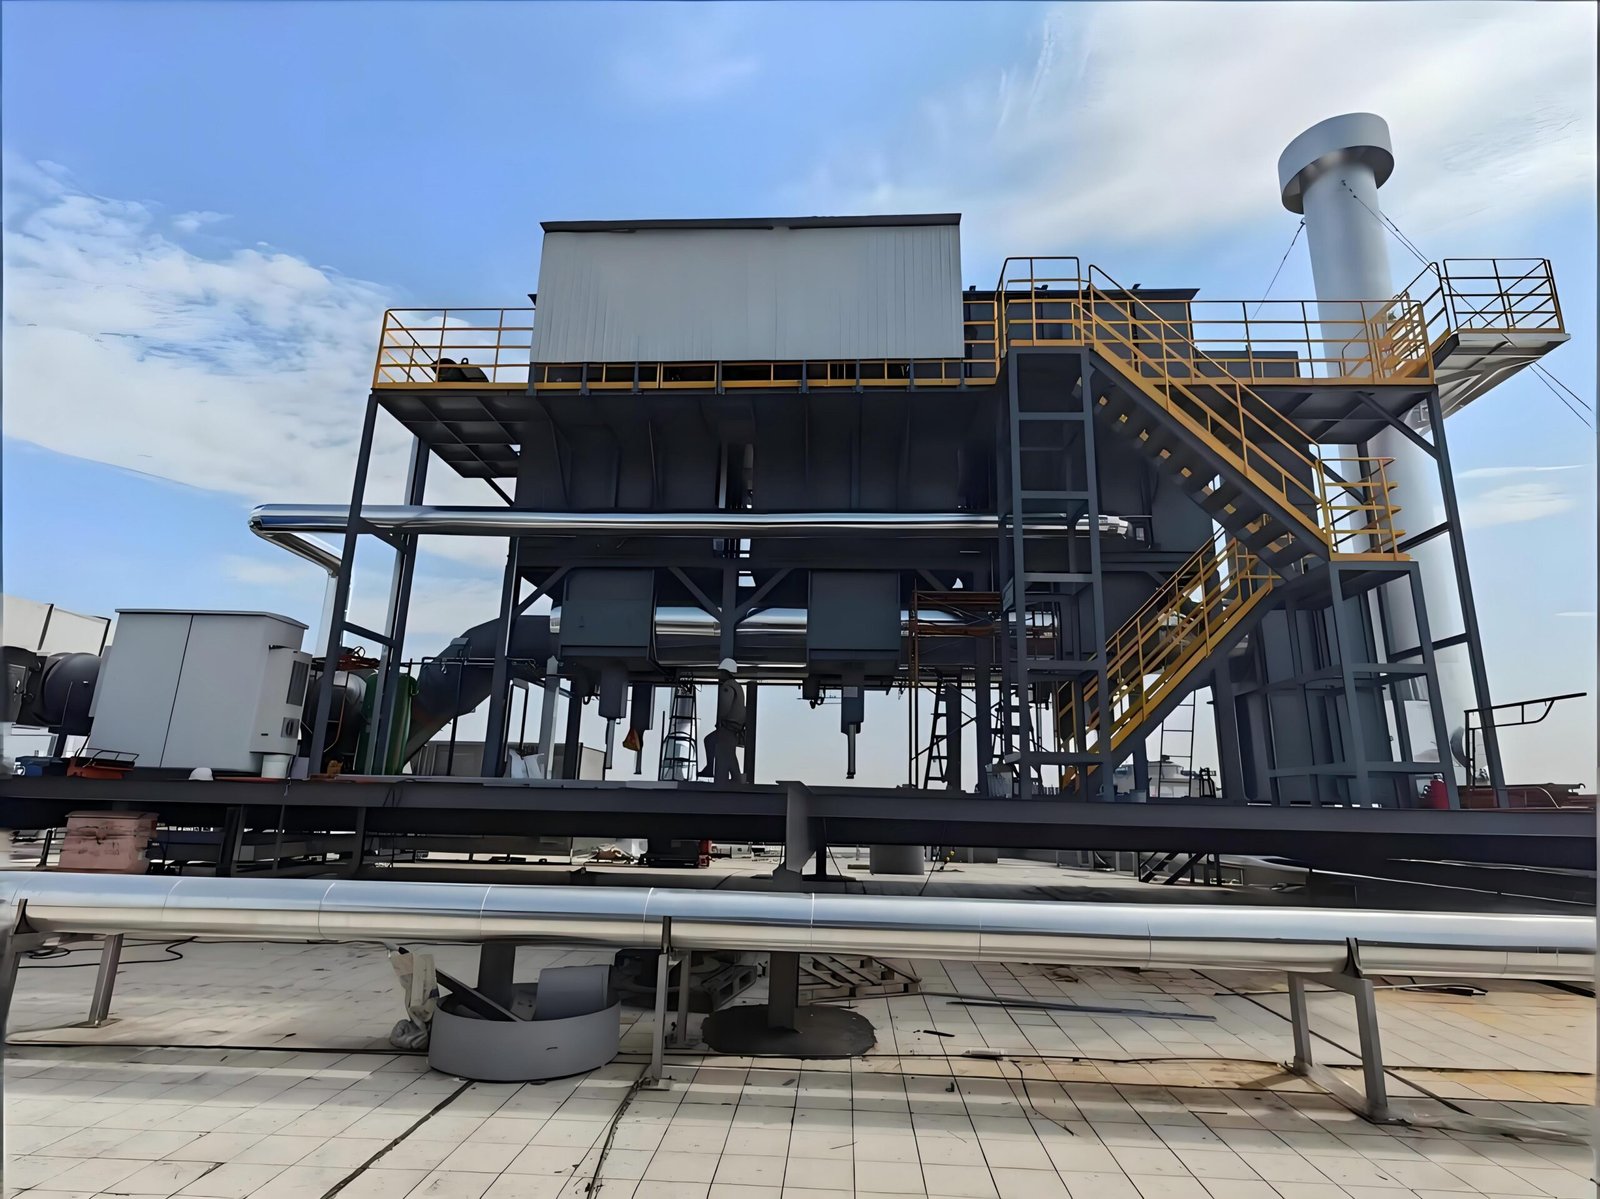
    Exterior regenerative thermal oxidizer equipment illustrating a critical-spares and preventive-maintenance review

    1. Rank parts by consequence, not by price

    Start with a consequence-and-recovery screen. A part deserves a higher criticality rank when its failure can stop the approved process route, create a safeguard concern, damage adjacent equipment, or extend recovery beyond the plant’s available maintenance window. Purchase price alone does not capture that exposure.

    Use a short review for every candidate item:

    • What function does the part perform in the gas path, thermal system, controls, or safeguard chain?
    • What is the credible failure mode: leakage, loss of position, loss of signal, wear, fouling, thermal damage, or electrical failure?
    • Can the equipment run in an approved alternate mode while the part is sourced?
    • Is the exact configuration identifiable from a drawing, tag, serial number, or approved data sheet?
    • What is the realistic restore-and-test time, including inspection and commissioning checks?

    The result is a ranked list that maintenance, EHS, operations, and procurement can understand together.

    2. Use a criticality matrix that procurement can act on

    A simple matrix helps the team distinguish an item that should be held on site from one that can be ordered after inspection. Adapt the categories to the site’s operating and safety procedures.

    CriticalityTypical consequenceEvidence to retainPlanning response
    A – operation or safeguard criticalLoss may stop an approved operating case or make a required safeguard unavailableTag, exact model/configuration, failure mode, approved substitute status, test methodConfirm availability, storage condition, and escalation contact before the maintenance window
    B – recovery criticalUnit may remain available but recovery is delayed by a unique or long-lead componentDimensions, materials, revision, supplier lead time, repair optionHold a repairable spare or written sourcing plan with a trigger date
    C – routine wear or consumableFailure is predictable and replacement is usually straightforwardConsumption history, inspection interval, compatibility notesSet reorder point and include in planned work packs
    D – common hardwareLocal or standard replacement is possible without changing the approved designStandard, size, material, and drawing referenceVerify local source and keep specification under document control

    Do not assign a criticality class permanently. A process change, new source, altered control strategy, or supplier discontinuation can move an item to a different class. Review the matrix whenever the RTO configuration or operating case changes.

    3. Separate assemblies from the parts that actually fail

    Supplier quotations often list a complete valve, burner, fan, or instrument assembly. That is useful for scope, but it may hide the field-replaceable items that cause most maintenance delays. Break each assembly into the parts that require different evidence and lead-time decisions.

    For a valve package, the review may include the body, seat or seal set, actuator, position feedback, solenoid, limit switches, mounting hardware, and any actuator-specific calibration or setup tool. For a burner package, consider the burner hardware, ignition components, flame-sensing device, combustion-air items, and gaskets as separate records when the approved documentation treats them separately. For a fan, record the bearing arrangement, coupling or belt configuration, vibration or temperature sensor, and any special balancing requirement.

    This decomposition prevents a common purchasing mistake: holding a generic spare that physically fits but cannot be commissioned or verified in the installed control and safety chain.

    4. Preserve configuration evidence with every spare record

    The most valuable spare is not only the metal part. It is the part plus the evidence that proves where it belongs and how it must be checked. Store the approved equipment tag, manufacturer and model, revision, material or temperature rating where relevant, dimensions, connection details, serial or batch information when required, and the drawing or manual reference.

    Add a clear photo only as supporting evidence; do not use an image as the sole identification method. Record whether the item is new, repaired, refurbished, or removed for inspection. Note shelf-life, protective packaging, preservation requirements, and environmental limits according to the supplier or site procedure.

    For control and safety components, retain the approved parameter set, firmware or revision requirement where applicable, and the post-installation test or proof-test reference. Do not assume that a visually identical component is an approved substitute.

    5. Ask lead-time questions before the work order is urgent

    Lead time is more than the number of calendar days quoted for shipment. The purchasing record should expose the assumptions that can change that number.

    Ask the supplier:

    1. Is the quoted lead time for a new item, a repair exchange, or a factory inspection?
    2. Which information must be confirmed before the order enters production?
    3. Is the quoted configuration tied to a drawing revision, serial number, or control-system version?
    4. Are critical materials, coatings, seals, sensors, or actuators sourced separately?
    5. What is the realistic dispatch date, and what events could move it?
    6. Is an approved substitute available, and what site verification is required before use?
    7. What inspection, calibration, leak check, stroke test, or functional test is expected after installation?
    8. Can the supplier provide an outline drawing, certificate of conformity, test record, or preservation instruction required by the plant’s document process?

    Get these answers before the outage window is fixed. A short written clarification can prevent a long delay caused by a missing dimension, obsolete revision, or unplanned test.

    Industrial workshop and machinery context for documenting RTO spare-part condition and inspection evidence

    6. Match stock decisions to failure evidence and recovery options

    Avoid both extremes: stocking every imaginable item and keeping no unique item at all. Use the failure history, inspection findings, operating exposure, and recovery options to decide what should be on site, repairable, consigned, or sourced on demand.

    DecisionSuitable whenControl needed
    Hold installed spareConsequence is high and sourcing or testing exceeds the available recovery windowVerify preservation, revision, and periodic condition review
    Hold repairable exchangeThe failed item can be removed and sent for repair while an accepted exchange restores serviceDefine acceptance test, turnaround assumption, and ownership
    Supplier-held or consigned stockThe item is unique but the supplier can guarantee access and configurationConfirm reservation, response time, storage responsibility, and expiry review
    Order after inspectionFailure mode and local availability make rapid sourcing realisticMaintain an approved specification and trigger point
    No stock; engineering review requiredA substitute or design change may affect safety or approved operationDefine escalation and prohibit informal substitution

    The decision should be visible in the maintenance system and linked to the RTO tag. An unlabelled box in a storeroom is not a controlled spare strategy.

    7. Build a maintenance-ready parts review

    Before a planned maintenance window, conduct a short cross-functional review. Operations confirms the operating case and outage constraints. Maintenance checks access, removal tools, lifting, permits, and test capacity. Engineering confirms configuration and approved alternatives. Procurement confirms availability, commercial terms, and delivery assumptions. EHS or process-safety personnel review any safeguard or hazardous-area implications within their role.

    The review should produce a work-pack list with part status, evidence status, owner, and decision date. Mark unknowns explicitly. If the team cannot confirm a model, revision, or test method, the action is to retrieve the evidence, not to guess from a similar photograph.

    After the work, update the record with the installed part identity, removed-part disposition, inspection findings, test results, and any new condition evidence. This closes the loop between preventive maintenance and the next procurement decision.

    FAQ

    Which RTO parts are usually considered critical spares?

    There is no universal list. Parts that can interrupt an approved gas path, burner or fan function, valve sequencing, measurement, or required safeguard may be critical for one installation and less critical for another. Rank them using consequence, uniqueness, failure evidence, and restore-and-test time.

    Should we stock a complete valve or only seal kits?

    Use the installed failure modes and recovery window. A seal kit may be adequate when the body and actuator are reliable and the repair can be tested locally. A complete exchange may be justified when configuration is unique or the repair and test path is longer than the available outage window.

    How can we verify that a substitute part is acceptable?

    Do not rely on physical fit alone. Confirm the approved specification, materials, temperature and pressure limits where relevant, interfaces, control parameters, and required functional or safety tests with the responsible engineering and supplier teams.

    How often should a critical-spares list be reviewed?

    Review it at a defined site interval and whenever the RTO configuration, process sources, control strategy, failure history, or supplier availability changes. A new exhaust source or a revised control component can change criticality.

    Does SERNO provide a fixed spare-parts package for every RTO?

    No universal package can represent every installation. A useful package depends on the actual equipment tags, operating case, maintenance evidence, approved documentation, and local recovery requirements. SERNO can help organize those questions for a technical review.

    Conclusion

    An RTO spare-parts strategy should make recovery decisions visible before a component fails. Rank items by consequence and lead time, separate assemblies into field-relevant parts, preserve configuration evidence, and define the inspection and test path alongside the purchase decision. That discipline helps a plant avoid both uncontrolled substitutions and unnecessary emergency stock.

    For an installed RTO or a planned maintenance program, SERNO can review the available equipment records, operating scenarios, and procurement questions for a site-specific technical discussion. Final operating, safety, and compliance decisions must follow the actual installation documents and qualified site procedures.

  • RTO Post-Restart Baseline Data: What to Record Before You Call It Normal

    RTO Post-Restart Baseline Data: What to Record Before You Call It Normal

    RTO Post-Restart Baseline Data: What to Record Before You Call It Normal

    Introduction

    After an RTO returns from a planned shutdown, maintenance event, or process interruption, the first steady operating period is valuable. It is the moment when the plant can distinguish a documented change from an unexplained shift in the exhaust-treatment train. That distinction is easily lost when teams record only a final “running” status.

    A restart baseline is not a universal set of numbers. It is a controlled record of how a specific system behaves in a defined operating state: which process sources are connected, what production is doing, which fan and control modes are active, and what the relevant instruments indicate. Without that context, comparing a warm-up reading with a peak-production reading can produce a false alarm—or hide a real one.

    This article is intended for the period after the installed shutdown and restart procedure has been completed and process exhaust has been admitted in an approved sequence. It does not replace OEM instructions, site operating limits, permit conditions, functional testing, or qualified safety review. Use those documents as the controlling requirements.

    Exterior regenerative thermal oxidizer equipment used to illustrate a post-restart operating-baseline review

    1. Treat “normal” as a defined operating case, not a single number

    The most useful baseline is tied to a repeatable operating case. For example, a plant may define one record for a single coating line at an established production rate and another for a combination of sources that normally run together. The record should identify the case clearly enough that a future shift can compare like with like.

    Start by writing the context beside the numbers. Include source identity, product or process state where relevant, approximate load condition, fan/control mode, date and time, weather or ambient condition if it materially affects the installation, and any active maintenance workaround. If a value was copied from a display, estimated, or unavailable, label it. An apparently precise baseline built from mixed-quality data is not a reliable reference.

    Avoid a blanket instruction to “return to last settings.” A changed process mix, an altered duct configuration, a new damper position, or a repaired instrument can make a prior display value unsuitable as a current target.

    2. Build the baseline in phases after process admission

    The first minute after ignition or fan start is often not representative of normal operation. Build the record in phases so the team can see whether the system is settling, drifting, or reacting to an added source. The exact timing must follow the installed procedure and site controls; the point is to identify the operating state, not impose a generic wait time.

    A practical recording sequence

    1. Equipment-ready observation: Record the approved mechanical and controls release, active alarms, fan status, valve feedback status, and the conditions before process exhaust is admitted.
    2. Initial process admission: Identify the first source or approved low-risk case. Record the relevant fan, pressure, temperature, and alarm observations after the system reaches the procedure-defined observation point.
    3. Representative operating case: Once the agreed production condition is established, capture the full baseline set and confirm which sources are actually connected.
    4. Load change observation: When a normal source is added or removed, note the resulting response. This creates context for later investigations without pretending that every fluctuation is a fault.
    5. Handover record: State the final system configuration, open actions, and who accepted the record.

    The baseline should not be used to bypass an interlock, prove compliance, or substitute for a required test. Its purpose is to preserve the evidence that makes later troubleshooting faster and more defensible.

    3. Record the variables that explain one another

    An isolated reading rarely explains a system change. A pressure increase may be associated with airflow, damper position, a blocked path, valve behavior, a changed source combination, or a measurement problem. A temperature trend may be linked to process loading, cycle state, sensor condition, burner response, or heat-recovery behavior. Record related variables together.

    Data groupExamples to capture where installedWhy the context matters
    Operating caseConnected sources, process state, approximate production condition, planned abnormal eventsMakes the comparison repeatable rather than generic
    Gas-path conditionFan mode or speed, relevant damper/valve feedback, pressure readings, access-door status after work releaseHelps separate airflow and routing changes from treatment-core questions
    Thermal and combustion observationRelevant temperature trends, burner state, cycle status, fuel indication where availableShows whether a change aligns with a different operating state or needs review
    Safeguards and controlsActive alarms, permissive state, instrument tag/status, manual or automatic modePrevents a bypass or temporary control state from being treated as normal
    Measurement qualityCalibration/verification status where applicable, unavailable channels, estimated values, time sourceAvoids false comparisons caused by uncertain data
    Maintenance and process changesWork completed, component replaced, duct/damper changes, product or solvent changePreserves the possible causes that are otherwise forgotten by the next shift

    Do not add variables merely because another RTO uses them. The installed configuration determines what is meaningful. A site should follow its approved tags, process safety information, and control narrative.

    4. Check data quality before interpreting a deviation

    Before treating a changed number as an equipment problem, check whether the comparison is valid. Was the same process combination running? Was the instrument available and plausibly reading? Did a maintenance task change the location, range, or control mode? Is the time stamp aligned with the actual source change? Has a temporary bypass, manual command, or abnormal production condition been disclosed?

    This is not an argument to dismiss deviations. It is a way to avoid changing a protective or operating setting before the team has identified what the reading represents. If a measurement is questionable, record it as questionable and follow the site’s instrument or maintenance process. Do not silently replace it with an assumed normal value.

    A simple comparison rule

    Compare a current observation only when the operating case, data source, and observation point are sufficiently alike. If they are not alike, classify the record as a new operating case or an incomplete comparison rather than drawing a conclusion from it.

    Industrial RTO duct and stack path supporting a post-restart baseline and deviation review

    5. Classify deviations so that action matches uncertainty

    Not every difference requires the same response. A useful restart log separates expected, explained changes from unexplained conditions and makes ownership visible. The categories below are a communication tool, not a substitute for site alarm limits or escalation procedures.

    Deviation classExample descriptionAppropriate next action
    Explained operating differenceA documented source combination or approved production condition differs from the prior baselineRecord the context and establish a separate comparable case if it will recur
    Measurement uncertaintySignal is unavailable, implausible, recently worked on, or its quality is unknownFlag the record, use the approved instrument process, and avoid treating it as a confirmed trend
    Stable but unexplained differenceComparable case shows a persistent pressure, temperature, or control-response changeAssign technical review; check work records, gas path, controls, and process context before adjustment
    Safety or procedure concernRequired safeguard state, alarm response, or approved operating condition is not availableFollow the site escalation and operating procedure; do not normalize the condition
    New process conditionProduct, solvent, airflow, duct route, or source use has changedUse the applicable management-of-change and engineering review process

    The value of the log is not its format. It is the discipline of writing why a difference is thought to be acceptable, who made that determination, and what evidence remains missing.

    6. Create a baseline record that the next shift can actually use

    A one-page template is often more useful than a large data dump. It should point to the historian, control trend, or work order where available, then summarize the essential operating case and exceptions. Use units exactly as the installed documentation uses them and avoid converting values casually in a handover note.

    Post-restart baseline record

    FieldRecordNotes
    Date, time, and observerIdentify the observation window and responsible role
    Operating case IDList connected sources and process state
    Restart/work referenceLink to the approved procedure, work release, and relevant maintenance notes
    Fan, valve, and control stateState automatic/manual condition and any approved temporary status
    Key process and RTO observationsRecord only installed, relevant tags with units and trend window
    Alarms, permissives, and exceptionsInclude “none observed” only for the defined observation period
    Comparison basisIdentify prior comparable record or state why no comparison is valid
    Deviation class and ownerState action, due date, and escalation route when needed
    Handover acceptanceRecord the accepting role and unresolved limits on routine operation

    Where a baseline is maintained in a digital historian or production record, a concise handover note should still point to it. A future investigator needs to know which trend window corresponded to a representative operating case.

    7. Do not let a temporary workaround become the baseline

    Restart periods can create pressure to resume production quickly. That makes undocumented manual commands, bypassed indications, temporary damper positions, or unexplained setpoint changes particularly risky as future reference points. A unit that is running is not automatically operating in its approved envelope.

    If the record exposes repeated alarms, unusual valve feedback, persistent pressure differences, unstable burner behavior, unexpected temperature response, or a process change that was not reviewed, preserve the evidence and use the site escalation path. For targeted checks, SERNO’s articles on RTO shutdown and restart, valve leakage diagnosis, and ceramic-media fouling can help structure the technical questions. They do not override the installed system documentation.

    FAQ

    How soon after restart should we collect the RTO baseline?

    Collect observations at the procedure-defined stages, then retain a representative record after the agreed process condition is established. There is no universal time interval: equipment configuration, process behavior, and site procedures determine the correct observation points.

    Should we use the pre-shutdown baseline as the restart target?

    Use it as a comparison reference only when the operating case and measurement quality are comparable. Documented maintenance, production, ambient, duct, or process changes may require a separate baseline rather than a forced return to an old number.

    What if a value has changed but there is no active alarm?

    An absent alarm does not explain the difference. Confirm the operating case and data quality, compare related variables, check documented changes, and assign review according to the site’s operating and safety process if the deviation persists.

    Can a supplier confirm that the RTO is operating normally from a remote baseline sheet?

    Not by the sheet alone. A qualified determination depends on the actual installation, installed limits, operating procedures, process conditions, instrument condition, and applicable requirements. A well-structured record helps make that review more efficient.

    Conclusion

    The best time to establish an RTO baseline is before an unexplained change is accepted as normal. Record the operating case, related readings, data quality, completed work, and exceptions together. Then make deviations visible, comparable, and owned.

    For an RTO project or a plant reviewing its post-restart operating records, SERNO can help organize the available exhaust data, operating scenarios, equipment scope, and documentation questions for a technical discussion. Final operating, safety, and compliance decisions must be made for the actual installation by qualified personnel under the applicable site procedures and requirements.

  • RTO Shutdown and Restart Checklist: Preserve Equipment, Verify Readiness

    RTO Shutdown and Restart Checklist: Preserve Equipment, Verify Readiness

    RTO Shutdown and Restart Checklist: Preserve Equipment, Verify Readiness

    SEO title

    RTO Shutdown and Restart Checklist: Preserve Equipment, Verify Readiness

    Meta description

    Plan a controlled RTO shutdown and restart with a practical checklist for isolation, preservation, inspections, controls, burner checks, process admission, and records.

    Slug

    `rto-shutdown-restart-checklist`

    Excerpt

    A planned RTO outage is not complete when the burner is off. This engineering checklist helps plant teams preserve the system while idle, inspect the gas path and safeguards, and restart in a controlled sequence before process exhaust is admitted.

    Introduction

    An RTO may be shut down for a production holiday, a planned maintenance window, a process change, or a utility outage. Turning off the burner is only one part of that event. The unit, duct network, induced-draft fan, valves, instruments, controls, and connected production sources can all be affected while the system is idle.

    The return to service deserves the same discipline. A stable cabinet indication or a successful burner light-off does not by itself prove that the complete exhaust-treatment train is ready for process gas. Water ingress, condensation, a valve left isolated, an unbalanced damper, an instrument that has drifted, or a changed process solvent can alter the conditions assumed when the RTO was last operating.

    This article provides a practical framework for a planned shutdown and restart. It is not a substitute for the installed system’s operating manual, site permit, lockout/tagout procedure, or a qualified safety review. Use the OEM documentation and site procedures as the controlling documents, then adapt the checklist to the actual RTO configuration and process hazards.

    Outdoor regenerative thermal oxidizer equipment prepared for a planned shutdown and preservation review

    1. Define the outage boundary before the final process stop

    Start with a short outage plan that states why the RTO will be stopped, how long it is expected to remain idle, which process sources will be isolated, and who owns each release decision. Treat the RTO as a train, not a single box. The boundary may include hoods, branch ducts, dampers, pretreatment, fans, the oxidizer, heat recovery, stack equipment, fuel supply, compressed air, electrical panels, drains, and monitoring points.

    Record the last stable operating conditions before shutdown. Useful evidence commonly includes airflow, pressure drop, relevant temperatures, fan speed or damper position, burner status, valve-cycle status, alarm history, fuel indication where available, and the active process combination. These values are a baseline for restart investigation; they are not universal performance targets.

    The plan should also identify credible changes during the outage. A new product, altered production schedule, duct modification, solvent change, or maintenance action can turn a routine restart into a management-of-change review.

    Shutdown planning questions

    • Which sources must be empty, purged, or isolated before the exhaust train is taken offline?
    • What energy sources, stored pressure, hot surfaces, and moving equipment require site lockout/tagout controls?
    • Which valves, dampers, drains, access doors, and temporary blanks must have a positive position record?
    • What condition needs protection during a short idle period versus a long or humid-season shutdown?

    2. Shut down in a controlled sequence and preserve evidence

    Follow the installed operating sequence and plant safety procedure. In many configurations, the process exhaust is removed first, the unit completes its specified purge or cool-down behavior, and utilities are isolated only when the system documentation permits it. Do not infer a safe sequence from a different RTO model: chamber arrangement, valve configuration, controls, upstream process, and local safeguards matter.

    Before releasing the equipment, document the final configuration. A simple signed status sheet can capture isolation points, damper positions, access-door status, temporary work controls, open maintenance items, and the person responsible for removal of each lock or tag. Photographs may help local teams, but they should support rather than replace a controlled isolation register.

    Avoid leaving a vague instruction such as “restart after holiday.” The next shift needs to know what was intentionally changed, what was found, and what has not yet been verified.

    3. Protect the idle RTO from water, contamination, and unintended movement

    Idle equipment can degrade quietly. Inspect weather protection and drain paths around roofs, ducts, stacks, fan housings, access covers, and low points. Water or condensation can affect insulation, corrode ductwork, foul instrumentation, damage electrical components, and create difficult-to-explain behavior during the next heat-up.

    Preservation actions should be based on outage duration and site conditions. Depending on the installed configuration and OEM instructions, they may include securing access covers, protecting open ductwork during maintenance, managing drains, preventing dust ingress, maintaining specified enclosure conditions, and protecting control equipment from moisture. Do not seal a system in a way that defeats a required vent, creates a trapped hazard, or conflicts with site safety procedures.

    Check for contamination introduced by adjacent work. Welding debris, blasting media, insulation fibers, overspray, cleaning chemicals, or unsecured tools can create restrictions or safety concerns in the gas path. If process dust, mist, silicone-containing materials, halogens, sulfur compounds, or other contaminants are relevant, the inspection scope should reflect the actual risk to ceramic media, catalyst where installed, instruments, and downstream equipment.

    4. Inspect the gas path, fan, valves, and access points before energizing

    The restart inspection should trace the actual gas path from collection point to stack. Confirm that the work boundary has been cleared and that all covers, blanks, guards, expansion joints, flexible connections, supports, drains, and access doors are in their correct service condition. Review any maintenance records for changes to duct routing, damper settings, fan components, valve seals, or insulation.

    Pay particular attention to items that change pressure balance or permit unintended air entry. An access door that is not seated, a damper left in a temporary position, a leaking valve, or an obstructed drain can affect operation even when the RTO reaches temperature normally. Where the system history includes pressure-drop or valve concerns, compare the post-restart readings with the pre-shutdown baseline and investigate meaningful differences rather than adjusting setpoints immediately.

    AreaVerify before restartWhy it matters
    Collection and branch ductsIsolation removed as planned; hoods and dampers returned to approved positionsSupports intended capture and airflow distribution
    RTO chambers and media pathAccess closed; no foreign material; maintenance work releasedAvoids leakage, restrictions, and damage
    Switching valves and actuatorsMechanical condition, air supply, feedback, and commanded movement checked per procedureValve position affects purge, heat balance, and gas routing
    Fan and motorGuards, rotation check method, vibration condition, electrical protection, and drain condition reviewedThe fan determines capture and system pressure
    Stack and downstream equipmentAccess, drainage, supports, heat recovery or polishing equipment checked where installedConfirms the full discharge path is available
    Industrial fabrication area supporting an RTO restart-readiness review

    5. Prove controls, interlocks, and combustion readiness without assuming

    Before process gas is admitted, verify the control system according to the approved functional test procedure. Confirm that required instruments have power, plausible readings, correct tags, and current calibration or verification status where applicable. Review alarms, permissives, emergency-stop functions, fan proving, valve feedback, pressure switches, temperature signals, gas-train safety functions, and any concentration or LEL safeguards specified for the installation.

    Combustion-system checks must follow the burner manufacturer’s instructions and be performed by personnel qualified for the task. A restart after fuel-system work, electrical work, a long shutdown, or an unexplained prior trip may require a more formal review. Do not bypass a permissive merely to obtain ignition. A bypass can hide the condition that should prevent a startup.

    The objective is not to claim a particular destruction efficiency or fuel rate. It is to demonstrate that each safeguarding and control function needed for the approved operating envelope is available before the exhaust source is connected.

    6. Restart in stages: equipment first, then controlled process admission

    A staged restart separates mechanical and controls questions from process questions. First, complete the documented equipment-start sequence without process exhaust, as the installed procedure allows. Observe fan, valve, temperature, burner, pressure, and alarm behavior during the warm-up and initial cycles. Record the conditions and compare them with the prior stable baseline, allowing for documented differences in ambient temperature, production state, or maintenance changes.

    Next, admit process exhaust in a controlled order. Start with the agreed source or low-risk operating case, then add sources only after the team confirms capture, pressure, temperatures, and safeguards remain acceptable. Avoid combining first restart, peak production, solvent changeover, and unfamiliar process conditions in the same moment. When the process profile has changed, pause for a qualified engineering and safety review rather than treating the event as a normal restart.

    Practical staged-restart record

    StageWhat to recordRelease criterion
    Mechanical readinessWork release, guards, access covers, utility availabilityAll listed shutdown controls cleared by the responsible owner
    Controls and burner readinessPermissive tests, signal plausibility, alarm status, combustion test resultApproved procedure completed with no unresolved safeguard issue
    Warm-up and cycle observationTemperature trend, valve operation, fan/pressure behavior, abnormal alarmsBehavior consistent with approved procedure and investigation of any deviation
    First process admissionSource identity, operating state, airflow/pressure observations, relevant process informationCapture and RTO response remain within the agreed operating envelope
    Return to routine operationFinal configuration, open items, baseline comparison, handover name/timeResponsible team accepts documented operating status

    7. Close the event with records that make the next decision easier

    The most valuable restart record is usable at the next outage. Keep the shutdown sheet, work releases, inspection findings, maintenance changes, alarm notes, final operating observations, and unresolved items together. Note which readings are measured, estimated, or unavailable. This prevents a future team from treating a temporary workaround or unusual baseline as normal design intent.

    If the restart exposed persistent pressure change, repeated valve alarms, unstable combustion, unexpected temperature behavior, or a process-source change, identify the follow-up owner and due date. A return to production is not evidence that the root cause has been resolved.

    FAQ

    How long can an RTO remain shut down?

    There is no single answer. The acceptable idle period depends on the installed equipment, environment, preservation method, process contamination, and OEM/site requirements. Plan the preservation scope around those conditions rather than relying on a generic number of days.

    Can we restart the RTO before checking the process ducts?

    The RTO may be capable of warming up, but the complete exhaust train should be released through the approved procedure before process gas is admitted. Unreleased access points, changed dampers, water, or temporary work controls in the duct system can affect capture, pressure, or safety.

    Should we change setpoints when readings differ after restart?

    Not as the first response. Compare the difference with maintenance activity, ambient conditions, process state, instrument condition, and the pre-shutdown record. Determine the cause through the approved engineering process before changing a protective or operating setting.

    What should an RTO buyer ask a supplier to provide?

    Ask for the installed system’s shutdown, preservation, and restart guidance; functional-test requirements; list of required utilities and instruments; and the information needed to assess a future process or duct change. The final procedure must match the supplied configuration and site controls.

    Conclusion

    A planned RTO outage is a controlled change in operating state. Preserving the equipment, confirming the full gas path, testing safeguards, and admitting process exhaust in stages helps a plant separate normal restart behavior from a condition that needs investigation.

    For a planned RTO project or an installed system facing a process change, SERNO can review the available exhaust data, operating scenarios, equipment scope, and documentation needs for a technical discussion. Any final operating, safety, and compliance decision must be made against the actual installation, applicable requirements, and qualified site procedures.

    Internal-link and pre-publication notes

    • Suggest contextual links to SERNO articles on RTO safety interlocks, valve leakage diagnosis, and ceramic-media fouling after their URLs are verified on the live site.
    • Keep the canonical self-referencing. Do not add unverified local permit, performance, customer, certification, pricing, or energy-saving claims.
  • Adding a New Exhaust Source to an Existing RTO: The Change-Management Review Before You Connect It

    Adding a New Exhaust Source to an Existing RTO: The Change-Management Review Before You Connect It

    An existing regenerative thermal oxidizer (RTO) can appear to have spare capacity: the nameplate airflow may be higher than the current reading, the combustion chamber may be stable, and a new production line may only run part of the day. None of those observations alone proves that a new exhaust source can be connected safely or reliably.

    The proposed tie-in changes a system rather than simply extending a duct. It can alter total airflow, VOC mass loading, oxygen conditions, inlet temperature, moisture, particulate carryover, pressure losses, combustion demand, valve cycling, fan duty, alarm logic, and the way operating data should be interpreted. The risk is not limited to an undersized oxidizer. A poorly defined connection can create unstable collection at one source, high static pressure, loss of capture, nuisance trips, an unreviewed flammability scenario, or a performance question that cannot later be explained from the data.

    For plant engineers, EHS managers, project managers, and technical buyers, the practical question is: what must be checked before a new exhaust source is allowed to join an existing RTO? The answer is a documented change-management review based on the actual combined operating envelope—not a comparison of one new flow number with a nameplate value.

    Existing industrial RTO equipment and ductwork reviewed before adding a new exhaust source

    1. Define the change as an operating scenario, not a duct connection

    Start with a one-page description of the change. Identify the new process, each pickup point, the collection method, the duct route, intended operating hours, expected start-up and shutdown sequence, and whether the source can run simultaneously with existing sources. Include what happens during cleaning, solvent changeover, upset, maintenance, bypass, and emergency stop.

    This scope should distinguish between design assumptions and measured evidence. For example, a supplier data sheet may state a nominal exhaust flow, while field measurements may show a different range once dampers, hoods, doors, or process speed are considered. Treat the range and the operating combinations as the review input. Do not reduce the proposal to an average flowrate.

    A useful scenario matrix lists the normal combined case, the high-flow case, the high-VOC case, start-up, low-production operation, a source isolated for maintenance, and any credible upset. It gives every discipline the same basis for review.

    2. Recheck combined airflow and the collection system

    The RTO is only one part of the gas path. The review should trace air from the new hood or enclosure to the stack, including branch ducts, balancing dampers, manifolds, fans, any pretreatment, the RTO inlet, heat-recovery equipment where present, and the outlet route.

    For each scenario, compare the combined airflow range with the verified operating range of the existing system. Then examine the collection side: adding a branch can redistribute flow away from existing hoods if the pressure balance changes. A new source may receive too little capture flow even if the RTO itself is thermally capable of treating the gas. Conversely, forcing more flow through a common header can increase static pressure and reduce performance at multiple pickup points.

    Request or create a current duct and instrument diagram, then mark the proposed connection, isolation point, balancing point, measurement locations, and control points. If current field data are unavailable, identify the gap explicitly and plan baseline measurements before final equipment selection.

    Questions to answer

    • What are the minimum, normal, and maximum flows at each source under representative production conditions?
    • Which sources can operate together, and which are mutually exclusive?
    • Does the added branch change capture performance at existing hoods or enclosures?
    • What is the fan operating point before and after the tie-in, including a reasonable allowance for fouling and damper position?
    • Is there a practical method to balance, measure, and document the new branch after commissioning?

    3. Evaluate VOC loading, composition, and flammability together

    Airflow does not describe the thermal or safety effect of a new source. The review should characterize the expected VOC constituents, concentration range, temperature, oxygen content where relevant, moisture, and contaminants that may affect ceramic media, catalysts, ducts, fans, or instruments. Separate routine process emissions from intermittent releases such as solvent flushing, manual cleaning, batch transitions, or abnormal conditions.

    The important engineering input is the combined loading profile. A source with modest airflow may still materially change combustion demand or the safety envelope if its concentration peaks when other sources are active. The reverse can also be true: a high-volume, low-concentration stream may change fan and heat-balance behavior more than oxidation duty.

    Flammability evaluation must be performed by qualified personnel using the actual mixture and the agreed plant safety basis. Do not assume that a low average concentration represents every operating condition. The review should confirm how the new stream is handled by the system’s existing monitoring, permissives, dilution strategy, alarm setpoints, isolation logic, and emergency response procedures. Where information is incomplete, use conservative operating controls until a qualified assessment establishes the permitted envelope.

    4. Check pressure loss, fan margin, and temperature effects

    New ductwork introduces pressure loss, but the bigger question is where the loss appears in the complete system. Review duct diameter, transitions, elbows, dampers, silencers, filters or pretreatment stages, access doors, and the tie-in geometry. Verify the fan curve, motor rating, variable-speed range where applicable, and the system curve for the relevant combined cases.

    Also consider temperature. Exhaust temperature affects gas density, volumetric flow at the fan, condensation risk, material selection, and the thermal behavior of the RTO. A hot new source can change upstream conditions; a cooler or moisture-rich stream can change the balance differently. If the system includes heat recovery or downstream treatment, its allowable conditions belong in the review too.

    Avoid treating a fan’s motor nameplate as proof of usable margin. The verified duty point, control range, vibration condition, and electrical protection settings matter. A fan operating close to its limit may not provide stable capture after a new branch is opened.

    5. Review the RTO, utilities, and downstream equipment as one train

    Confirm the proposed envelope against the actual configuration of the installed RTO: chamber arrangement, valve sequence, combustion system, temperature instrumentation, purge arrangement, operating logic, and any agreed limitations in the operating documentation. The review should determine whether the source changes residence-time assumptions, bed temperature balance, burner support requirement, reversal behavior, or planned maintenance window.

    Utilities deserve the same attention. A source addition can change electricity demand through fan operation, fuel demand during low-loading periods, compressed-air demand for valves or instruments, and drain or condensate requirements. If dilution air, a bypass, carbon polishing, scrubber, heat recovery, or a stack fan is part of the current train, assess its capacity and control interaction as well.

    This is not a promise that an RTO will meet a particular removal result or fuel consumption after a tie-in. Those outcomes depend on the verified gas profile, equipment condition, operating strategy, and applicable permit requirements. The purpose of the review is to make the constraints and verification methods clear before the connection is built.

    Industrial workshop environment used for an RTO commissioning and change-management review

    6. Update controls, interlocks, and operating procedures before energizing the branch

    An added source should appear in the system documentation and operating logic, not only on a construction drawing. Review whether the new branch requires a position feedback signal, damper interlock, flow indication, process-run signal, VOC monitor interface, temperature override, or a different start/stop sequence. Define what action occurs if the branch is opened while the RTO is unavailable, if a fan trips, if a high-temperature or high-concentration condition occurs, or if a process signal is lost.

    Changes to safety-related logic must follow the plant’s management-of-change and functional-safety procedures. The team should identify who approves the logic, who tests it, and how the test record is retained. Operators and maintenance personnel need a clear procedure for normal operation, isolation, lockout, abnormal alarms, and re-start after intervention.

    A practical pre-tie-in checklist

    Review areaEvidence to collect before approvalWhy it matters
    Process definitionSource list, operating modes, material/SDS information, start-up and upset descriptionSets the real combined envelope
    Airflow and captureField readings or a measurement plan, hood/duct layout, simultaneous-operation matrixProtects collection performance and fan stability
    VOC and contaminantsRepresentative composition/range, temperature, moisture, particulate or mist concernsSupports thermal, materials, and pretreatment review
    Safety basisQualified flammability review, existing monitor/interlock coverage, emergency actionsPrevents assumptions about peak events
    Mechanical scopeTie-in drawings, isolation and balancing points, supports, access, drainageMakes the modification maintainable and testable
    Fan and utilitiesFan/system curves, motor/control data, utility capacity checkAvoids an unworkable operating point
    Controls and documentsRevised P&ID, cause-and-effect, procedures, training and test recordKeeps the installed change aligned with operations
    Acceptance planBaseline and post-tie-in test plan, responsibilities, data log and review criteriaProvides traceable completion evidence

    7. Commission with baseline and post-change evidence

    Before the physical tie-in, capture a baseline for the current system under defined production conditions. Record the operating scenario, airflow or pressure measurements at agreed points, fan speed or load where available, RTO temperatures, valve/fan status, utility readings, alarm history, and any relevant emissions-monitoring data under the site’s established method. A baseline does not eliminate engineering calculations; it makes later changes easier to interpret.

    After commissioning, repeat the planned measurements with the new source isolated and with the agreed combined cases. Confirm that capture remains effective, dampers can be balanced, the fan operates within the reviewed range, controls perform as intended, and any required plant or regulatory verification is completed by the appropriate parties. Document deviations and corrective actions rather than silently redefining the acceptance condition after the fact.

    For a broader introduction to early data collection, see What Are VOCs in Factory Exhaust? A First Check Before Choosing Treatment Equipment and How to Estimate Factory Exhaust Airflow for a First VOC-Treatment Inquiry. For a system-scope perspective, link to What Makes Up a Complete RTO System? Look Beyond the Main Oxidizer. Confirm final URLs before publishing these internal links.

    FAQ

    Can we connect a new exhaust source if the current RTO has unused nameplate airflow?

    Possibly, but nameplate airflow alone is not enough. The decision should consider actual combined flow, capture balance, fan capacity, pressure loss, VOC loading, safety controls, temperatures, utilities, and the installed configuration.

    Do we need to sample the new exhaust before the change?

    The appropriate sampling approach depends on the process, local requirements, and engineering scope. At minimum, establish representative information on constituents, concentration range, temperature, moisture, and intermittent conditions so the change can be evaluated. Use qualified professionals for sampling and safety assessment where required.

    Is a new branch damper sufficient to control the added source?

    A damper may be part of the solution, but it does not prove airflow balance, safe operation, or control integration. The design should include a documented balancing and verification approach.

    When should the management-of-change review be completed?

    Complete it before finalizing the tie-in design and before the new source is energized. This allows duct, fan, controls, utility, and safety issues to be resolved while the modification is still practical to change.

    Professional CTA

    Planning to add a process exhaust source to an operating RTO or VOC-treatment line? Share the source list, operating scenarios, available airflow/VOC information, current drawings, and the proposed tie-in concept with SERNO. We can help structure a technical review scope for your project. Final equipment suitability, safety assessment, and compliance decisions should be confirmed against verified site data and applicable local requirements.

  • What Makes Up a Complete RTO System? Look Beyond the Main Oxidizer

    What Makes Up a Complete RTO System? Look Beyond the Main Oxidizer

    What Makes Up a Complete RTO System? Look Beyond the Main Oxidizer

    When a factory begins a VOC-treatment project, it is easy to ask for an “RTO.” But an RTO main unit is not the entire system.

    A practical project has to move real exhaust from the process to a defined treatment route, manage the interfaces around that route, and provide a safe, maintainable operating boundary. What is included depends on the process, exhaust condition, site layout, and local requirements.

    This guide is a plain-English scope map for first-time buyers. It is not a design, permit decision, safety assessment, or performance guarantee.

    Start with the exhaust source and collection boundary

    The system begins where exhaust is generated: a process hood, enclosure, dryer connection, tank vent, or another capture point. Duct branches and dampers then bring the proposed stream toward treatment.

    Collection is not a background detail. Poor capture can leave emissions outside the system; uncontrolled branch changes can make the treatment duty unclear. Map sources, airflow estimates, operating periods, and normal versus non-routine events before treating the oxidizer as the whole project.

    For a first data list, see VOC Exhaust Data Checklist Before RTO Quotation and What Are VOCs in Factory Exhaust?.

    Conditional upstream protection: pretreatment is part of the scope conversation

    Some streams can carry dust, fibers, mist, oil, resin, condensable material, or corrosive components. If those materials may reach the downstream equipment, the project may need upstream protection, different materials, changed collection, or a different treatment route.

    Generic industrial VOC treatment installation with ductwork, access platform, stack, and process modules

    There is no universal pretreatment train. The right question is: what actually enters the duct under production, cleaning, changeover, and upset conditions? The answer should be based on process information and, where appropriate, qualified engineering review.

    Read Which Industries May Be a Fit for RTO? for an early explanation of why an industry label alone cannot answer that question.

    The RTO main unit: the treatment core, not the entire project

    The regenerative thermal oxidizer is the treatment core of an RTO route. It commonly combines heat-recovery media chambers, a combustion section, flow-reversal equipment, insulation, access points, and instrumentation. Exact configuration is project-specific.

    The main unit should be discussed alongside its incoming stream, operating schedule, utilities, controls, service access, and discharge path. A stand-alone equipment drawing cannot confirm that the surrounding system interfaces are workable.

    Fans, ducting, and the discharge path connect the system

    Fans and ductwork move the exhaust through the defined path. Their practical scope may include branch connections, transitions, supports, dampers, isolation points, and access for inspection. A stack or discharge arrangement completes the downstream path, subject to local and site-specific review.

    These elements affect space, routing, noise considerations, maintenance access, and what is included in a supplier or site scope. See Industrial Exhaust Treatment Equipment for why dust, mist, acid gas, and VOC streams should not be assumed to share one route.

    Controls, safety functions, and utilities make the scope operable

    A treatment system needs an agreed control boundary. That may include a control panel, field instruments, operating statuses, alarms, interlocks, and interfaces to the factory process. The detailed logic and safeguards must be established for the actual project; they are not interchangeable from one line to another.

    Utilities also need early confirmation. Depending on the route, that can include electrical supply, fuel, compressed air, drainage, foundations, and access around equipment. Listing an oxidizer without these interfaces can create scope gaps later.

    A complete RTO system scope map

    System blockWhat to define earlyWhy it belongs in the same discussion
    Capture and collectionSources, hoods, ducts, branches, operating scenariosDefines what is actually delivered to treatment
    Conditional pretreatmentDust, mist, oil, condensables, corrosive componentsHelps protect the downstream route and clarify boundaries
    RTO main unitProcess duty, configuration discussion, access needsThe treatment core must match the defined stream
    Fan, duct, and stack pathRouting, supports, discharge arrangement, spaceConnects the real process to and from the main unit
    Controls and safeguardsOperating interfaces, alarms, project-specific logicMakes the equipment operable within the plant boundary
    Utilities and civil/site worksPower, fuel, air, drainage, foundation, accessOften affects schedule, responsibility, and budget scope

    The table is a scoping aid, not a standard equipment list or a compliance conclusion.

    Five questions to ask before requesting an RTO proposal

    1. Where are all relevant exhaust sources, and which run at the same time?
    2. What is known about airflow, VOC materials, temperature, moisture, dust, mist, and unusual events?
    3. What collection, pretreatment, utilities, civil work, ducting, and stack items are already on site—and what must be included?
    4. Who will define the controls and operating interfaces with production equipment?
    5. Which local permit, testing, safety, and discharge requirements need qualified confirmation?
    Generic modular industrial treatment equipment with ductwork, a fan, control enclosure, and exhaust stack

    FAQ

    Is the RTO main unit the same as a complete RTO system?

    No. The main unit is central, but collection, stream conditioning where needed, duct/fan/stack connections, controls, utilities, and site works can be part of the broader project scope.

    Does every RTO system need pretreatment?

    Not necessarily. It depends on the actual inlet condition. The decision should follow a review of what could enter the collection system, not a generic diagram.

    Can a supplier quote the RTO before all data are available?

    An early budgetary discussion may be possible, but unknown data and unclear scope boundaries should be stated clearly. A final configuration needs project-specific review.

    What should a buyer prepare first?

    Prepare a process/source list, available material or SDS information, airflow estimates, operating schedule, photos or layout drawings, utility information, and notes about dust, mist, deposits, odor, or corrosion.

    Build the system boundary before comparing equipment

    SERNO can help structure an early discussion around the exhaust sources, stream data, collection boundary, conditional pretreatment, main treatment route, utilities, and site interfaces. Share the available project information through the SERNO RTO page or contact form. Final design and local-requirement decisions need project-specific engineering review.

    Sources and retrieval note

    For general background, consult the applicable local authority and qualified advisors. The U.S. EPA Stationary Sources of Air Pollution overview was checked on 2026-07-29 as general background only; it is not cited as a requirement outside the United States.

  • Which Industries May Be a Fit for RTO? Start With Exhaust and Pretreatment

    Which Industries May Be a Fit for RTO? Start With Exhaust and Pretreatment

    Which Industries May Be a Fit for RTO? Start With Exhaust and Pretreatment

    Plant teams often ask, “Is our industry suitable for an RTO?” It is a reasonable first question—but the industry name is only a starting point.

    An RTO, or regenerative thermal oxidizer, may enter the discussion where a factory has an organic VOC exhaust stream and a treatment project can be defined around the real operating pattern. The answer depends on what leaves the process, how it is captured, how often the line runs, and what else travels in the duct.

    This guide is general orientation for first-time buyers. It is not a system design, permit decision, safety assessment, or performance guarantee.

    RTO suitability begins with the exhaust pattern, not the factory label

    Two factories in the same sector can have very different treatment needs. One may run a steady, well-captured stream; another may have intermittent batches, cleaning events, mixed branches, or visible aerosol.

    Before an RTO route can be assessed, document the proposed inlet: VOC composition where known, airflow, schedule, temperature, moisture, dust, mist, and unusual events.

    For basic VOC context, see What Are VOCs in Factory Exhaust? and the industrial exhaust categories guide.

    Industries that may start an RTO feasibility discussion

    Spray coating, curing, and coated-product lines

    Coatings, thinners, cleaning materials, and cure/dry stages may create a defined VOC exhaust stream. That can justify an RTO feasibility conversation.

    Overspray, pigment-containing dust, sticky aerosol, changeovers, and cleaning periods still need their own review. A coating line is not automatically an RTO project just because solvents are used.

    Flexible packaging, printing, and converting

    Inks, solvents, laminating adhesives, and drying sections can lead packaging and converting teams to investigate VOC treatment. Map each relevant source and distinguish normal production from wash-up, changeover, and start/stop conditions.

    See the printing and flexible-packaging VOC guide for sector detail. Capture and upstream contaminants still need review.

    Resins, adhesives, chemical processing, and formulated materials

    Batch mixing, coating, impregnation, reaction, drying, and solvent handling may produce VOC-bearing exhaust. Process records and material information matter because the duty can vary.

    Ingredients, corrosive components, or condensable material can change the route or upstream protection required.

    Composite materials, FRP, and related fabrication

    Composite layup, resin application, and curing can prompt a VOC-treatment review. Identify the sources, enclosure status, and any fiber, resin-droplet, or other carryover that could enter the ductwork.

    The practical question is not just “Does the process use resin?” It is “What reaches the collection point under normal and non-routine conditions?” Specialty manufacturing and pharmaceutical steps can need the same documented review, especially for batches, cleaning, and product changes.

    Why pretreatment is an early boundary—not an optional afterthought

    Treatment equipment only receives what the capture system and ductwork deliver. If the stream contains materials that can foul, corrode, condense, or otherwise affect downstream equipment, the scope may need upstream protection or a different treatment route.

    Technical rendering of a modular industrial oxidation system with ductwork, fans, access platform, and stack

    Common early-review items include:

    • Dust and fibers: can build up in ducts, filters, and downstream equipment.
    • Oil, resin, or coating mist: can deposit on surfaces and complicate maintenance.
    • High-boiling or sticky condensables: may cool and collect before they reach the intended treatment zone.
    • Acidic, alkaline, or corrosive components: may affect material selection and the overall route.
    • High or changing moisture: can alter the practical discussion around capture, condensation, and heat balance.
    • Mixed exhaust branches: may combine streams that should be characterized separately before a common treatment decision.

    This does not automatically prescribe a filter, scrubber, or standard pretreatment train. It is a reason to look upstream before choosing equipment.

    A simple industry-to-data checklist

    Process patternWhat to map before asking for an RTO proposalWhy it mattersPossible early scope question
    Coating or curingCoating/cleaning steps, hoods, overspray, line scheduleVOC vapor and aerosol may not behave the same way in collectionIs there mist or particulate carryover to control?
    Printing or convertingInk/adhesive use, dryer exhaust, wash-up, changeoversThe duty can vary through the production cycleWhich sources operate together, and when?
    Resin, adhesive, or chemical batchesMaterial list, vent sources, batch timing, temperature, cleaningComposition and flow can change by batch or productAre condensables or corrosive components possible?
    Composite fabricationResin application, enclosure status, fiber/dust sourcesCapture and physical carryover both need reviewWhat enters the duct besides vapor?
    Specialty manufacturingProduct campaigns, solvents, containment, abnormal eventsA single “average” may hide operational variationWhich scenario should define the design boundary?

    The table is a scoping aid, not a sizing chart or compliance decision.

    Outdoor industrial exhaust-treatment equipment with ductwork, service access, and control enclosures

    Five questions to answer before comparing RTO proposals

    1. Where is the VOC-bearing exhaust generated? Mark the sources, hoods, enclosures, and duct branches.
    2. What is known about the materials and operating schedule? Include normal production, changeovers, cleaning, and reduced-load operation.
    3. What else can enter the stream? Note dust, fibers, mist, oil, resin, acid/alkaline gas, or condensable material.
    4. What are the project boundaries? Clarify collection upgrades, pretreatment, electrical/gas utilities, space, access, stack, and controls—not just the oxidizer.
    5. Which local requirements must be checked? Confirm permit, testing, safety, and emission obligations with the relevant local authority and qualified advisors.

    For a broader first comparison of treatment routes, read Activated Carbon vs RCO vs RTO. It explains why no equipment acronym can replace a defined exhaust-data package.

    FAQ

    Is RTO suitable for every factory that uses solvent?

    No. Solvent use can justify a VOC-treatment review, but suitability depends on the actual stream, capture, operating pattern, contaminants, site constraints, and applicable requirements.

    Does every RTO project need pretreatment?

    Not necessarily. Evaluate what can reach the treatment equipment. The answer should come from the real stream, not a standard diagram.

    Are coating and printing always the best industries for RTO?

    They are common places to begin a VOC-treatment conversation, but neither is automatically a match. Process data and collection conditions still decide what needs review.

    Can one RTO handle exhaust from several processes?

    Possibly, but only after combined flow, timing, chemistry, contaminants, collection layout, and operating scenarios are reviewed.

    What should a first supplier conversation include?

    Bring a process list, material or SDS information where available, source locations, airflow estimates, operating schedule, photos or drawings of capture points, and notes about visible dust, mist, deposits, odor, or corrosion. It is fine if some information is still incomplete—state the gaps clearly.

    Start with a scoped exhaust review

    If your process may have a defined VOC exhaust stream, SERNO can help structure an early review around sources, operating pattern, capture, pretreatment boundaries, and site constraints. Share available data through the SERNO RTO product page or the site contact form. A final route needs project-specific engineering and local-requirement review.

    Sources and retrieval note

    Check air-emissions background against applicable official sources and local rules. The U.S. EPA’s Air Pollutant Emissions Trends Data page was accessible on 2026-07-28 and is cited only as general background, not as a requirement outside the United States.

  • Activated Carbon vs RCO vs RTO: How to Start Comparing VOC Treatment Routes

    Activated Carbon vs RCO vs RTO: How to Start Comparing VOC Treatment Routes

    Activated Carbon vs RCO vs RTO: How to Start Comparing VOC Treatment Routes

    When a factory first investigates VOC exhaust treatment, three names often appear quickly: activated carbon, RCO, and RTO. They are not interchangeable products, and a lower first-cost route is not automatically the simpler route over time.

    The useful question is not “Which one is best?” It is: which route fits the actual exhaust stream, operating pattern, capture arrangement, and project boundary?

    This guide gives a plain-English first comparison for teams preparing to speak with an equipment supplier. It is general orientation, not a design, permit decision, safety assessment, or performance guarantee.

    Technical rendering of a multi-chamber industrial oxidation unit with ductwork, platform, and stack

    First, what are these three routes?

    Activated carbon: capture by adsorption

    Activated carbon is commonly used to adsorb some organic vapors from an air stream. In simple terms, vapor molecules are held in the porous carbon material. The system therefore depends on suitable stream conditions and a plan for monitoring, changeout, regeneration, or other material management.

    It can be part of a VOC-control discussion where the exhaust and operating pattern are appropriate. It is not a universal “fit-and-forget” filter. Dust, mist, humidity, contaminants, concentration changes, fire/safety considerations, and the carbon-management plan all need project-specific review.

    RCO: catalytic oxidation with heat recovery

    RCO means regenerative catalytic oxidizer. It uses catalyst and regenerative heat recovery as part of an oxidation route for certain VOC duties. The catalyst is a key part of the process, so the actual compounds and possible contaminants matter.

    An RCO conversation should include more than airflow. Teams should discuss materials used, expected changes in production, upstream carryover, service access, and how the system will be operated. Do not assume every mixed or uncharacterized stream is suitable for catalytic treatment.

    RTO: thermal oxidation with heat recovery

    RTO means regenerative thermal oxidizer. It is another oxidation route, using thermal oxidation and regenerative heat recovery. It is often considered for some continuous industrial VOC streams, especially when the project has enough verified operating information to define the duty.

    RTO is not a shortcut around collection quality, pretreatment, site layout, utilities, or local requirements. Some streams may need upstream protection or a different route. A system discussion should always begin with the real stream, not the equipment acronym.

    For a closer two-technology discussion, see RTO vs RCO: How to Choose VOC Oxidation Equipment. This article is broader: it helps a new buyer decide what to ask before placing activated carbon, RCO, and RTO on the same shortlist.

    A practical first comparison

    RoutePlain-English functionWhat the buyer should clarify earlyOperating conversation to expectImportant boundary
    Activated carbonHolds some VOCs in porous mediaVOC type, moisture, dust/mist, concentration pattern, operating hoursMedia condition, monitoring, changeout/regeneration, safe material handlingA carbon bed is not automatically suitable for every vapor or mixed stream.
    RCOOxidizes certain VOCs using catalyst and heat recoveryStream chemistry, catalyst-sensitive contaminants, capture consistency, pretreatmentCatalyst protection, maintenance access, startup/shutdown patternCatalyst compatibility must be evaluated for the real stream.
    RTOOxidizes certain VOCs using thermal oxidation and heat recoveryFlow, concentration variation, production schedule, upstream carryover, site constraintsCollection, pretreatment, utilities, controls, maintenance accessAn RTO is not automatically the right answer for every flow, concentration, or schedule.

    This table is a decision-starter, not a sizing chart. It deliberately avoids a universal ranking because the same route can be sensible in one duty and a poor fit in another.

    Start with the factory’s operating pattern

    Two factories can use similar coatings or solvents yet need different project discussions. One line may run steadily through multiple shifts. Another may start and stop, run batches, or change products frequently. One site may already have disciplined source capture and clean ductwork; another may be dealing with leaks, mixed branches, or visible mist.

    The operating pattern affects the questions that matter: what is emitted, when it is emitted, how consistently it is captured, and what arrives at the treatment inlet. It also affects maintenance planning, material handling, utilities, controls, and the practical scope of installation.

    Before asking for a model or price, map the process and record normal production, reduced production, cleaning, changeover, and unusual operating periods. A proposal based on the wrong schedule or an incomplete stream description can create confusion later.

    Technical rendering of modular industrial exhaust-treatment equipment with ducting, a collection stage, fan, and stack

    Pretreatment and capture are part of the choice

    Treatment equipment only sees what the hood, enclosure, ductwork, and fan deliver to it. Poor capture can leave vapor in the workspace. Carryover of dust, fibers, aerosol, oil mist, or other materials can also change the downstream treatment discussion.

    That does not mean every project needs the same pretreatment train. It means the team should identify what can reach the equipment and whether a protection stage is needed. The right answer depends on the process and material information, not on a generic sales diagram.

    If your team is still determining whether the stream is VOC vapor, dust, mist, acid/alkaline gas, or a combination, begin with What Are VOCs in Factory Exhaust? and Industrial Exhaust Treatment Equipment: Match Dust, Acid Gas, Mist, and VOCs to the Right Route.

    What to prepare before a supplier conversation

    You do not need a complete engineering package to begin. A clear first data set is already valuable:

    1. A process list: coating, printing, adhesive, cleaning, drying, resin handling, or other relevant steps.
    2. Material names and available SDS documents for products used at each source.
    3. A sketch of hoods, enclosures, duct branches, fans, and any existing control equipment.
    4. Normal and peak operating schedule, including batches and product changeovers.
    5. Available airflow, temperature, and VOC information, clearly marked as measured, estimated, or unknown.
    6. Site constraints such as available space, access, utilities, discharge route, and local review requirements.

    SERNO’s VOC Exhaust Data Checklist Before RTO Quotation can help organize a more detailed handoff once the factory is ready for a scoped technical discussion.

    Four first-time-buyer mistakes to avoid

    1. Choosing by acronym alone

    “We need an RTO” or “we need carbon” is not yet a project definition. Treat the acronym as a starting point for questions, not as the answer.

    2. Treating airflow as the whole story

    Airflow is important, but it does not reveal the material, concentration pattern, moisture, carryover, or production timing. Those factors can change the route discussion.

    3. Leaving capture and pretreatment outside the scope

    The main unit, collection system, ductwork, fan, pretreatment, controls, and installation boundary should be discussed together. A well-chosen main unit cannot correct every upstream issue.

    4. Assuming a comparison table replaces local review

    Local permits, emissions obligations, safety requirements, and waste-handling responsibilities are site-specific. Keep the applicable local requirements with the project record and review them with qualified local parties.

    Which route should a factory investigate first?

    There is no responsible one-line answer without the stream information. As a practical next step, make a short comparison sheet for each route: what it needs from the incoming stream, what it needs from the site, what operating task it creates, and what is still unknown.

    If the stream has heavy dust, mist, unusual chemistry, frequent product changes, or unclear capture, resolve those questions before treating a route as selected. If the stream and schedule are stable enough to define, a supplier can give a more useful, clearly scoped discussion of activated carbon, RCO, RTO, or another approach.

    FAQ

    Is activated carbon always cheaper than RCO or RTO?

    Not necessarily over the life of a project. The appropriate comparison includes stream suitability, media management, operating pattern, installation scope, maintenance, and site-specific requirements. A price comparison without those boundaries can be misleading.

    Is RCO simply a smaller RTO?

    No. Both are oxidation routes, but the process approach is different and an RCO uses catalyst. The real VOC chemistry and possible catalyst-sensitive contaminants need evaluation.

    Can an RTO treat any VOC exhaust?

    No. RTO suitability depends on the actual stream, concentration behavior, contaminants, pretreatment needs, operating schedule, site conditions, and local requirements.

    What is the best first document to share with a supplier?

    Share the process list, material/SDS information, capture/duct sketch, schedule, available measurements, and site constraints. Mark assumptions and unknowns plainly.

    A clearer way to start a VOC-treatment project

    SERNO can help structure an early technical conversation around the information you are authorized to share: process, materials, capture arrangement, operating schedule, and site boundary. That conversation should clarify the route to investigate—not promise an outcome before the stream has been reviewed.

  • Industrial Exhaust Treatment Equipment: Match Dust, Acid Gas, Mist, and VOCs to the Right Route

    Industrial Exhaust Treatment Equipment: Match Dust, Acid Gas, Mist, and VOCs to the Right Route

    Industrial Exhaust Treatment Equipment: Match Dust, Acid Gas, Mist, and VOCs to the Right Route

    When a factory starts planning an exhaust-treatment project, it is tempting to ask for “one machine for the whole workshop.” The better starting point is: what is actually in each exhaust stream?

    Dust, acid or alkaline gas, oil mist, and organic vapor do not behave in the same way. They may need different collection methods, different pretreatment, and different treatment routes. One process can also produce more than one of them.

    This is a practical first guide for teams comparing industrial exhaust treatment equipment. It is not a permit decision, an exposure assessment, a performance guarantee, or a replacement for site-specific engineering.

    Start with the process, not the equipment name

    Walk the production route and note what leaves the process: a dry powder, droplets, a corrosive gas, a visible haze, a solvent vapor, or a mixture. Then connect each source to its hood, enclosure, duct, fan, or discharge point.

    For example, grinding may release particulate. A pickling or chemical process may release acid mist or gas. Machining can create oil mist. Coating, printing, adhesive use, cleaning, drying, or resin processing may release organic vapors, sometimes called VOCs.

    The same workshop can have several streams. Combining them without understanding the contents can complicate later treatment. A process sketch, material/SDS list, operating schedule, and existing duct layout are more useful than a broad equipment label.

    For an earlier VOC-only first check, see What Are VOCs in Factory Exhaust?. That guide is one part of the wider stream-identification step described here.

    Modular industrial exhaust treatment equipment with overhead ducting and an outdoor stack

    Four common exhaust categories

    1. Dust and dry particulate

    Dust is made of solid particles carried in air. It can come from cutting, sanding, grinding, mixing, conveying, trimming, or powder handling. The first questions are particle type, amount, size range, moisture, stickiness, and whether the dust has any special handling or safety considerations.

    Typical first routes can include source capture and a suitable particulate-collection stage. The correct collector, filter media, cleaning arrangement, disposal method, and safety measures depend on the real material. A dust collector is not automatically a VOC treatment system.

    2. Acid or alkaline gas and mist

    Acidic or alkaline emissions can arise from chemical processing, surface treatment, cleaning, etching, pickling, and similar steps. Some streams are gas-like; some include liquid droplets or mist. Their corrosive nature can influence duct materials, fans, drains, and downstream equipment.

    A wet collection or scrubbing route may be considered for some such duties, but the actual chemistry, concentration, liquid handling, and local requirements matter. A generic scrubber name is not enough to confirm suitability.

    3. Oil mist and process aerosol

    Oil mist is made of very small liquid droplets, often associated with machining, lubrication, forming, cooking, or other processes that create aerosols. It can appear as haze, deposit on ductwork, or accumulate on surfaces.

    The project team needs to distinguish mist from vapor and understand whether droplets, smoke, heat, or other contaminants are also present. Separation or filtration may be part of a route. If an oxidation system is later considered for an organic-vapor stream, upstream mist control can be important because the equipment must be protected from unsuitable carryover.

    4. Organic vapors (VOCs)

    VOCs are a category of compounds that can become vapor during manufacturing. Common source areas can include coating, printing, lamination, adhesive application, solvent cleaning, mixing, drying, curing, and resin handling. A smell can be a reason to investigate; it is not a measurement or a compliance conclusion.

    Potential routes for some organic-vapor duties can include source reduction, improved capture, adsorption, catalytic oxidation, thermal oxidation, concentration systems, or combinations. A regenerative thermal oxidizer (RTO) is commonly considered for some continuous VOC duties, but it is not an automatic answer for every flow, concentration, schedule, or mixed stream. Learn more about the selection discussion in How to Select an RTO System for VOC Abatement and the technology comparison in RTO vs RCO.

    A simple “stream to route” comparison

    What you see or recordFirst classification questionA route that may be consideredImportant boundary
    Dry powder or particlesWhat material, amount, and handling risk are involved?Source capture and particulate collectionA particulate collector does not by itself confirm VOC control.
    Corrosive gas or dropletsIs it gas, mist, or both? What chemistry is present?Capture plus a compatible wet or other treatment stageMaterials, liquid handling, and local requirements matter.
    Haze or oily depositsAre they droplets, smoke, vapor, or a mixture?Mist separation/filtration and source controlDo not send unsuitable carryover into downstream equipment.
    Solvent-like vapor from a processWhich materials, operating hours, and capture points are involved?Capture improvement, adsorption, oxidation, concentration, or a combinationSelection needs verified stream and site information.

    The table is an orientation tool, not a design specification. A professional review needs the actual process, materials, exhaust conditions, site constraints, and applicable local requirements.

    Industrial exhaust ductwork, fan housing, and stack at a rooftop treatment installation

    Why mixed streams need a staged discussion

    Many factories do not have a neat, single-contaminant exhaust stream. A coating or chemical process may include vapor, moisture, droplets, or particles. A shared duct can mix emissions from different operations. Pretreatment may therefore be part of the project, not an optional afterthought.

    Before connecting a new source to an existing system, document what is already captured and when each branch runs. The team should also identify any changes in material, production rate, line layout, or operating hours. This helps prevent a treatment decision from being made on incomplete assumptions.

    For a quotation-stage handoff, SERNO’s VOC Exhaust Data Checklist shows the kind of operating information that turns a general question into a more focused technical conversation.

    A five-item factory self-check

    1. List each process step that produces dust, mist, gas, or vapor.
    2. Record the raw material and available SDS for each source.
    3. Mark the capture point, duct branch, fan, and current control equipment.
    4. Note whether the source runs continuously, in batches, or only during certain shifts.
    5. Keep local permit, inspection, and emissions requirements with the project record for qualified review.

    Unknown values should stay marked as unknown. Do not invent airflow, concentration, removal performance, or compliance status in order to obtain an equipment comparison.

    FAQ

    Can one exhaust-treatment system handle every factory emission?

    Not automatically. Some sites have separate streams; others need a staged route. The answer depends on the actual contaminant mix, capture layout, operating pattern, compatibility, and applicable requirements.

    Does a scrubber remove VOCs?

    That cannot be assumed. Treatment depends on the actual compounds and stream conditions. Identify the contaminant and have the route assessed for the installed process.

    Can an RTO accept dust or oil mist directly?

    Do not assume so. Particulate, mist, moisture, and other carryover may create a pretreatment question. A site-specific review should establish what reaches the treatment unit and what protection is needed.

    What should we send before asking for a proposal?

    Share the process list, material/SDS information, capture and duct sketch, operating schedule, existing controls, known changes, and the local requirement you need to consider. Only provide information you are authorized to share.

    Choose the route after identifying the stream

    SERNO can help organize an early conversation around your process, materials, capture points, operating pattern, and available drawings. Send verified site information for a scoped technical review. Final technology selection, installation scope, and any compliance conclusion must be confirmed for the actual process and applicable local requirements.