Author: serno_admin

  • RCO Catalyst Temperature Profile: Diagnose Hotspots Before They Become a Shutdown

    RCO Catalyst Temperature Profile: Diagnose Hotspots Before They Become a Shutdown

    RCO Catalyst Temperature Profile: Diagnose Hotspots Before They Become a Shutdown

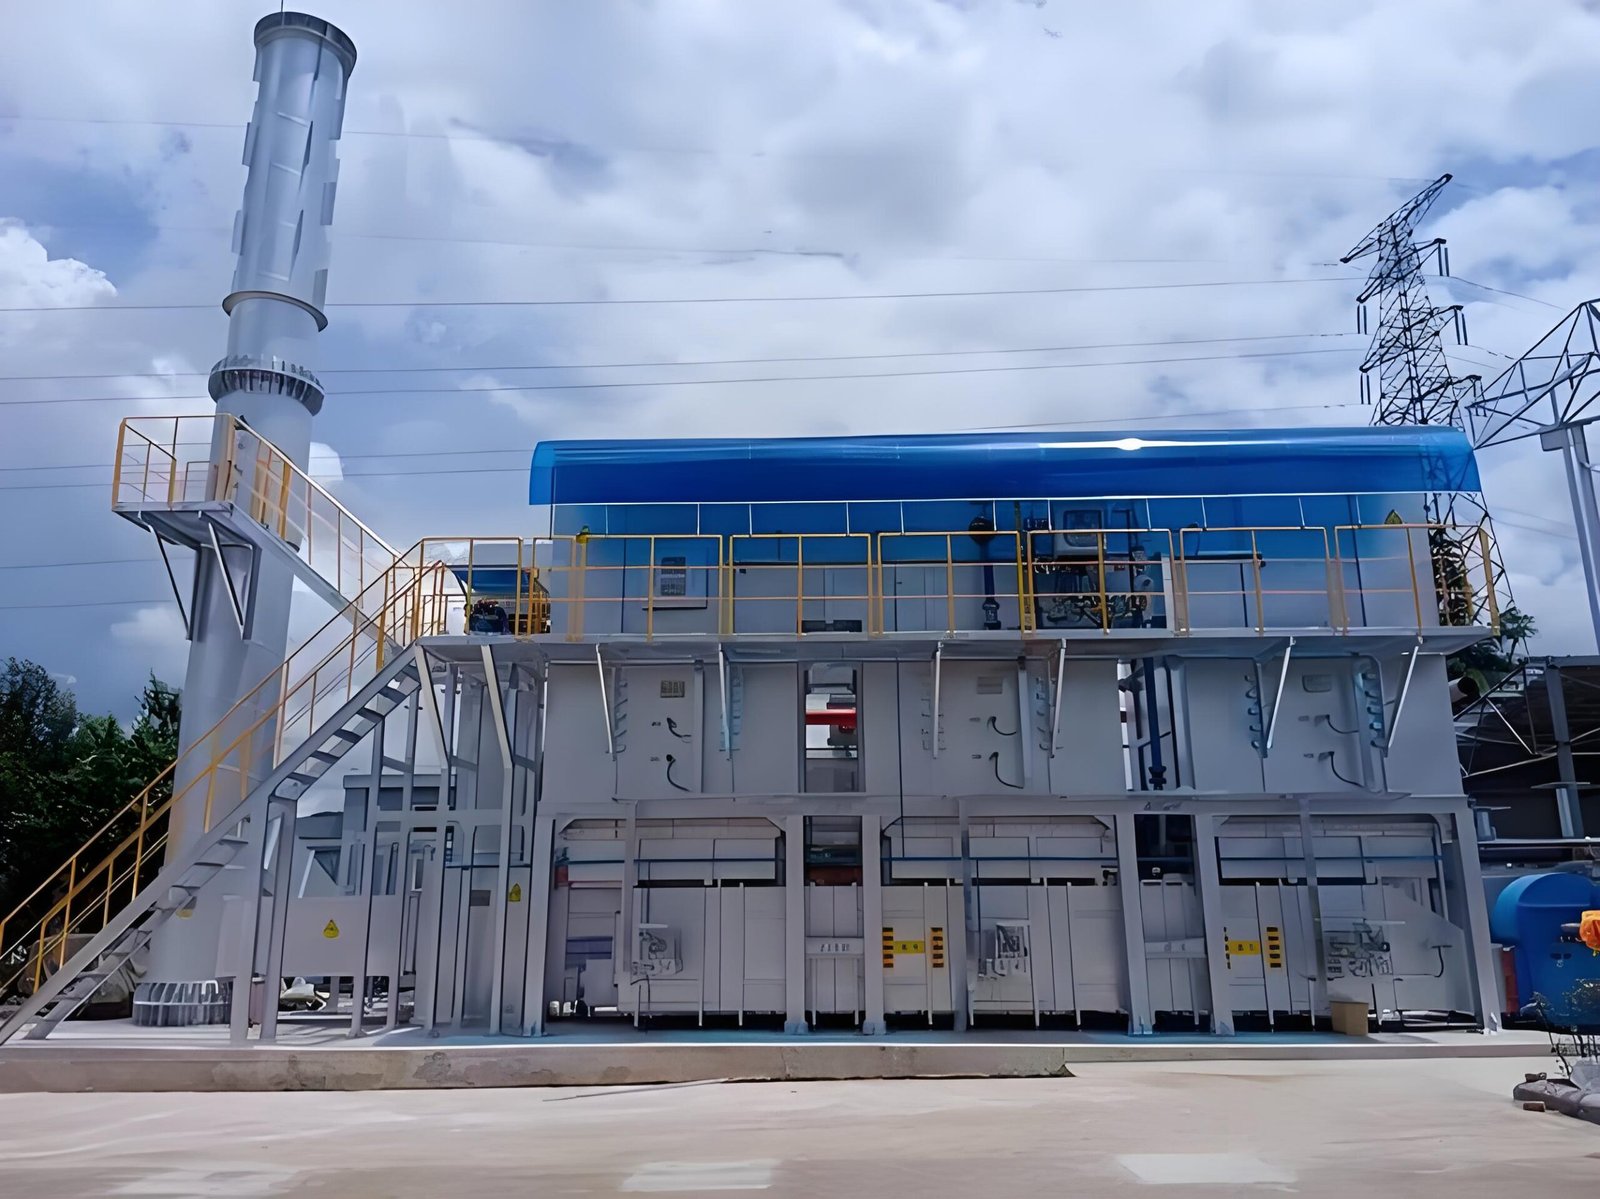
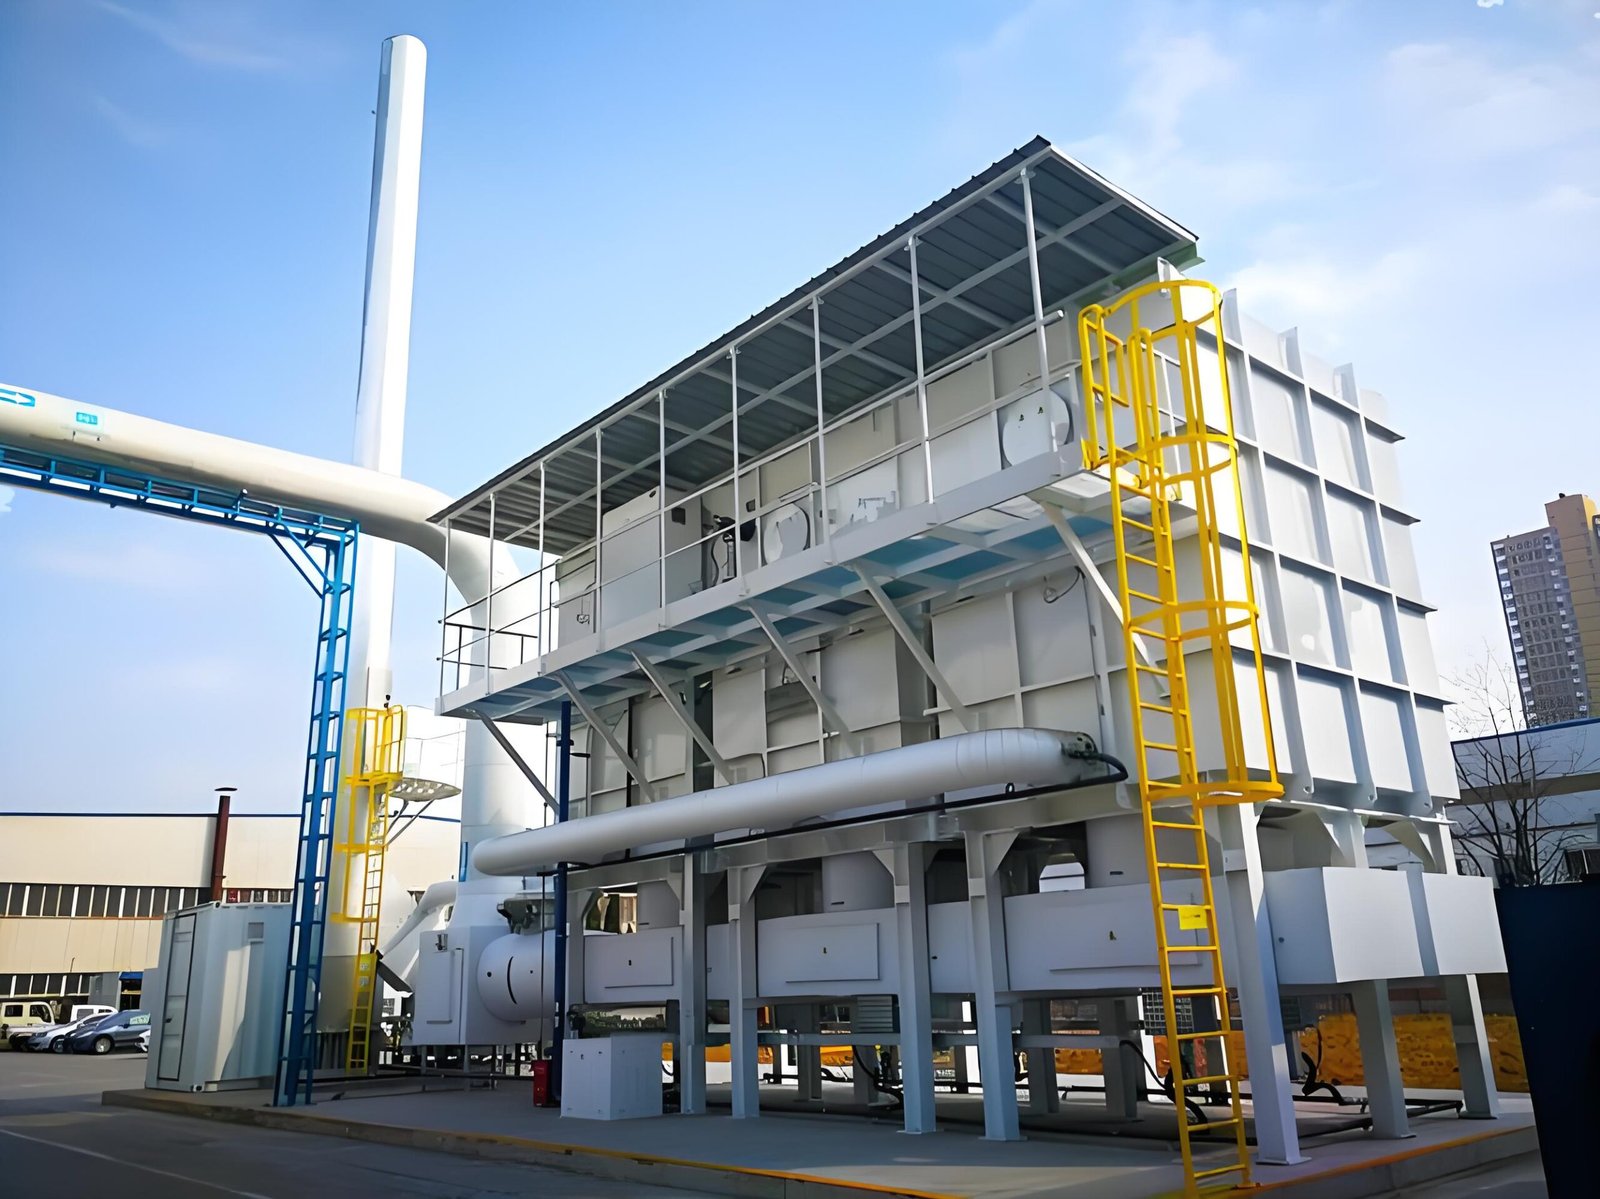
    An RCO reactor can show acceptable outlet readings while a local catalyst-bed hotspot is developing. A defensible diagnosis starts with a repeatable temperature profile, not a single display value. This guide explains how plant teams can collect comparable evidence, separate instrumentation error from catalyst or airflow problems, and define a safe next action.

    Engineer documenting Technician recording an RCO catalyst reactor temperature profile

    What a temperature profile can—and cannot—prove

    A profile shows how heat is distributed across the monitored boundary. It does not, by itself, prove catalyst activity, destruction efficiency, or a specific contaminant. Treat it as a screening and trend tool that must be interpreted with flow, VOC load, oxygen, pressure drop and operating-state records.

    Establish the measurement boundary

    Record sensor tag, location, insertion depth, calibration status, scan interval and reactor operating state. Compare upstream, bed-inlet, inter-bed where available, bed-outlet and exhaust temperatures using the same time window. Note whether the unit is ramping, switching, bypassing or at steady load.

    Build a repeatable profile sheet

    FieldMinimum record
    Operating statesteady, ramp, regeneration or bypass
    Process conditionsairflow, VOC load basis, oxygen, pressure drop
    Temperature pointstag, physical location, value and timestamp
    Instrument evidencecalibration date, alarm history, wiring check
    Contextrecent maintenance, solvent change, condensate or dust event

    Use the same points and sequence on every round. A trend becomes useful only when the measurement method is stable.

    Separate sensor problems from real hotspots

    First compare redundant sensors or a calibrated reference where the procedure allows. Check loose thermowells, drift, response lag, scaling and signal conditioning. A step change isolated to one channel is more consistent with instrumentation than with a full-bed thermal event. Do not defeat interlocks or enter restricted areas to obtain a reading.

    Interpret common profile patterns

    Localized high point

    A persistent high point can indicate uneven airflow, local VOC concentration, channeling or catalyst condition changes. Confirm the point across multiple steady-state rounds before escalating.

    Broad downstream rise

    A broad rise may reflect shifted reaction location, altered heat recovery or a changed load. Review airflow and VOC trend together rather than assigning the cause to catalyst age alone.

    Flattened or unusually cool profile

    Check sensor response, dilution air, bypass position and low-load operation. A cool profile is not proof that catalyst is inactive.

    Use corroborating evidence before opening scope

    Pair the profile with pressure drop, fan operating point, inlet concentration basis, oxygen, alarm history and maintenance records. If the profile changes after a process solvent or pretreatment change, preserve that timeline. For catalyst service decisions, request supplier-defined sampling or test criteria rather than relying on a visual impression.

    Define safe decision gates

    Escalate when a repeatable abnormal trend crosses the site’s approved alarm or operating limit, when redundant evidence agrees, or when the profile changes with unexplained process conditions. The response may be continued monitoring, instrument repair, airflow inspection, load reduction or a planned outage assessment. Site procedures and qualified personnel govern the final action.

    Questions to ask an RCO supplier

    • Which temperature points are included in the guaranteed monitoring boundary?
    • What calibration and replacement method is specified for each sensor type?
    • Which profile patterns trigger inspection, sampling or catalyst replacement review?
    • How are airflow maldistribution and pretreatment events separated from catalyst deactivation?
    Technician verifying an RTO burner low-pressure switch and valve feedback

    FAQ

    Is one high temperature reading enough to condemn the catalyst?

    No. Confirm the sensor, repeat the measurement and correlate the point with operating and process evidence.

    How often should a profile be recorded?

    Use the site’s risk-based procedure and record more frequently during commissioning, after process changes or when trends are unstable.

    Can temperature alone prove VOC destruction performance?

    No. Performance verification requires the site’s approved sampling and analysis method under defined operating conditions.

    Conclusion and CTA

    A disciplined RCO temperature profile turns an alarming display into evidence that maintenance and engineering teams can act on. SERNO can help define the measurement boundary, data sheet and inspection questions for an industrial VOC treatment review. Share your process range, airflow basis and current instrumentation map for a scoped discussion.
  • RTO Burner Gas-Pressure Verification: Prove Regulator Stability Before Ignition

    RTO Burner Gas-Pressure Verification: Prove Regulator Stability Before Ignition

    RTO Burner Gas-Pressure Verification: Prove Regulator Stability Before Ignition

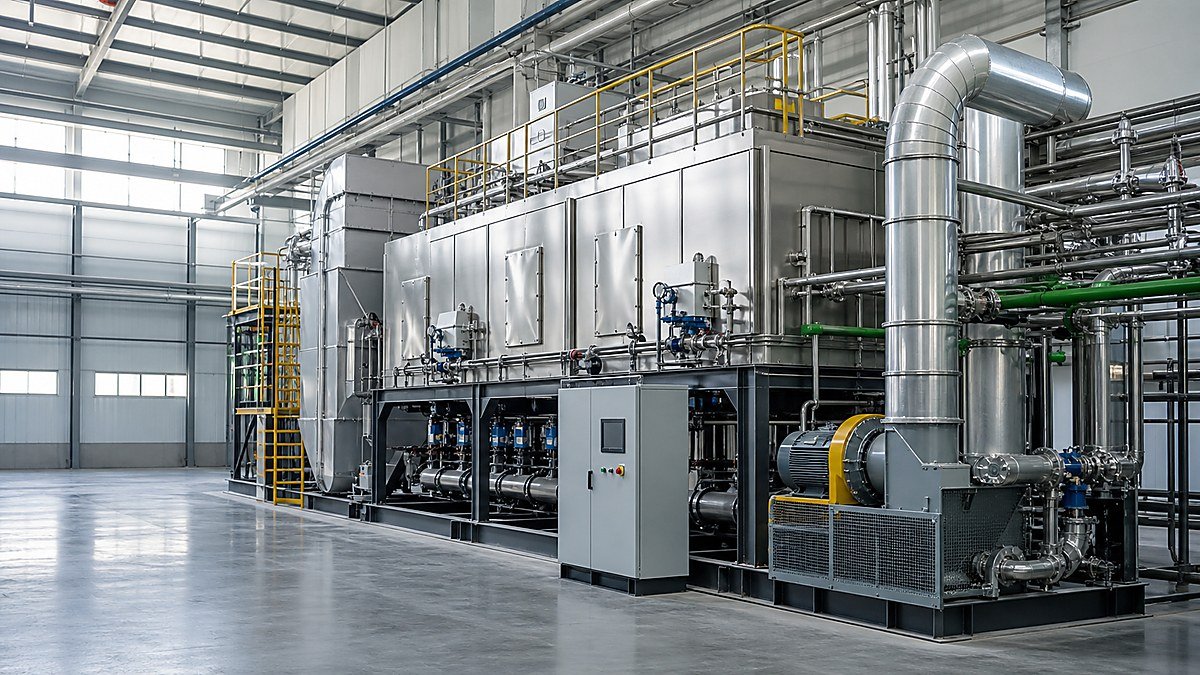
    An RTO burner can pass a leak test and still be unsafe to ignite if the regulator hunts, an impulse line is restricted, or a low-pressure switch is misaligned with the approved cause-and-effect. Gas-pressure verification should therefore be a controlled release activity, not a quick gauge reading. This guide helps plant EHS, commissioning and procurement teams define the evidence required before admitting fuel.

    Engineer documenting RTO burner gas-pressure verification beside regulator and tagged valves

    1. Define the pressure boundary and approved basis

    Collect the latest P&ID, burner data sheet, fuel specification, regulator data, valve-train arrangement and approved cause-and-effect. Mark the test boundary from the upstream isolation valve to the burner manifold. Record whether readings are gauge or absolute, the reference temperature, and the instrument tag. Do not substitute a generic pressure target for the supplier’s approved operating window.

    2. Verify instruments and impulse paths

    Use a calibrated test gauge or digital reference with a range suited to the service. Check calibration status, zero, manifold isolation and tubing support. Compare the local gauge with the control-system value at steady state. Inspect sensing lines for condensate, blockage, kinks and incorrect take-off points; a healthy regulator cannot compensate for a false signal.

    3. Test regulator response under controlled demand

    With the burner isolated from ignition, introduce the approved test medium and raise pressure gradually. Document upstream pressure, downstream pressure and time at each hold point. Repeat a controlled demand change (for example, pilot-only to the approved pre-purge condition) and record settling behavior, droop and rebound. Acceptance is stability within the approved vendor/engineering limits—not a universal number.

    4. Prove low-pressure protection and reset logic

    Use the approved test method to simulate a low-pressure condition. Confirm the switch or transmitter changes state, the fuel safety shutoff valves close, the burner permissive drops, and the alarm identifies the correct tag. Verify manual reset requirements and that loss and restoration of instrument power do not create an automatic fuel admission path. Record as-found and as-left setpoints; never adjust them without authorization.

    5. Capture a buyer-ready evidence pack

    Evidence rowMinimum recordRelease question
    BoundaryMarked-up P&ID and isolation listIs every fuel path included?
    InstrumentsTags, calibration dates, readingsCan readings be traced?
    RegulatorHold points and demand-response trendIs response stable in the approved window?
    TripsSimulated condition and valve feedbackDid the correct permissive drop?
    RestorationAs-left setpoints, leak check, signaturesIs the system safe to hand over?

    Store signed sheets, trend exports and deviation dispositions with the commissioning dossier. If a reading is outside the approved basis, stop the release and raise a technical query rather than hiding it in a general punch list.

    6. Release gates before ignition

    Ignition should require: completed boundary isolation, valid instrument checks, stable regulator response, witnessed trip test, verified valve feedback, cleared deviations and an authorized start permit. The first light-off should be observed with pressure, flame signal, oxygen and safety trips trending together. A pressure pass alone is not permission to ignite.

    Technician verifying an RTO burner low-pressure switch and valve feedback

    FAQ

    What pressure should an RTO burner have?

    Use the burner and regulator supplier’s approved operating window for the specified fuel. A generic value can be unsafe because trains and burners differ.

    How often should the low-pressure switch be tested?

    Test during commissioning, after train modifications and at the interval defined by the site’s safety-management and maintenance procedures.

    Can the PLC trend replace a calibrated gauge?

    No. Trend data is useful evidence, but it should be cross-checked against a calibrated reference instrument and a verified sensing path.

    What if regulator pressure hunts during the test?

    Hold ignition, check sensing lines, regulator sizing, supply stability and downstream demand, then document the root cause and corrective action before retesting.

    Talk with SERNO

    Share your fuel type, burner-train P&ID, instrument list and commissioning boundary with SERNO. We can help structure a verification matrix and evidence pack around your approved design basis—without guessing setpoints or bypassing site safety controls.

    Internal links: RTO burner fuel-train leak testing; RTO burner ignition sequence verification; RTO flame scanner verification before restart.

  • RTO Burner Fuel-Train Leak Testing: Evidence Before Ignition

    RTO Burner Fuel-Train Leak Testing: Evidence Before Ignition

    RTO Burner Fuel-Train Leak Testing: Evidence Before Ignition

    Fuel admission is a controlled change of risk, not a single valve operation. An RTO burner can have a correct ignition sequence yet remain unsafe if isolation valves, regulators, threaded joints or impulse lines leak. This guide helps plant teams define the test boundary, collect evidence and release the train only when independent checks agree.

    Engineer documenting an RTO burner fuel-train leak test beside tagged isolation valves

    1. Define the test boundary

    Mark the upstream isolation, regulator, double-block-and-bleed assembly, burner manifold, pilot branch and vent termination on one drawing. Record valve tags, normal position and the pressure rating of every component. Separate the fuel-side test boundary from combustion-air and purge circuits so a pressure change cannot be misread.

    2. Confirm instruments and test medium

    Use a calibrated pressure gauge or digital logger with a range suited to the test pressure. Record serial number, calibration due date, ambient temperature and test medium. Never introduce oxygen for a fuel-train tightness test. Follow the approved site procedure for nitrogen or the specified inert medium, then vent safely before fuel admission.

    3. Stabilize, isolate and observe

    Close the defined isolation valves, apply lockout where required and allow temperature to equalize. Pressurize in controlled increments, pause for stabilization, then record start pressure and time. Observe the hold period specified by the approved procedure; do not invent an acceptance limit from a generic internet checklist. Note pressure, temperature and any visible or audible indication at each interval.

    4. Check valve-seat and bleed behavior

    For double-block-and-bleed arrangements, prove each block valve separately and verify that the bleed path remains clear and terminates at a safe location. A rising pressure between blocks can indicate seat passing, trapped thermal expansion or an incorrectly aligned bypass. Photograph gauge readings and valve positions, and have a second competent person witness the critical steps.

    5. Localize any loss before repair

    If pressure decays beyond the approved criterion, stop and classify the result as failed. Use an approved leak-detection method at accessible joints, regulator vents and instrument connections. Do not tighten a live fuel joint. Repair under isolation, repeat the complete test boundary and retain both failed and passed records so the history remains auditable.

    6. Release gates before ignition

    The release pack should include the marked-up P&ID, valve lineup, instrument calibration, test log, repair record, vent confirmation and independent sign-off. Confirm purge permissives, flame-safety trips and emergency shutdown signals separately. Only then authorize fuel admission under the plant’s permit-to-work and startup procedure.

    Evidence checklist

    RecordMinimum evidence
    BoundaryTagged drawing and valve lineup
    InstrumentID, range, calibration status
    TestMedium, start/end readings, times, temperature
    BleedVent route and clear-path confirmation
    ExceptionsLeak location, repair and retest link
    ReleaseTwo-person sign-off and permit reference
    Technician checking valve seating during an RTO fuel-train test

    FAQ

    Is a pressure hold alone enough?

    No. It must be tied to a defined boundary, calibrated instrument, temperature context and valve-seat checks.

    Can operators tighten fittings during the test?

    No. Stop, isolate, depressurize and follow the site’s repair and retest process.

    What should buyers request from an RTO supplier?

    Request the test boundary, procedure reference, instrument records, raw readings, deviations and final release sign-off.

    CTA

    SERNO can help buyers turn burner fuel-train verification into a clear commissioning and handover evidence pack. Share your fuel-train P&ID and startup constraints for a scoped technical review.

  • RTO Burner Ignition Sequence Verification: Prove the Start-Up Logic Before Restart

    RTO Burner Ignition Sequence Verification: Prove the Start-Up Logic Before Restart

    RTO Burner Ignition Sequence Verification: Prove the Start-Up Logic Before Restart

    A burner can have a healthy refractory lining and a responsive flame scanner yet still start unsafely if the sequence logic, purge timer or permissive chain is wrong. Before an industrial regenerative thermal oxidizer (RTO) returns to service, verify the complete ignition sequence against the approved cause-and-effect narrative and record evidence at each gate.

    Engineer verifying an RTO burner ignition sequence beside the fuel train

    Why sequence verification matters

    The sequence coordinates isolation, purge, air proving, ignition, fuel admission and flame proving. A written “sequence complete” message is not enough; the team should know which input allowed each transition and which trip removed fuel.

    1. Freeze the approved sequence

    Collect the latest PLC logic revision, cause-and-effect matrix, P&ID references and burner vendor instructions. Mark any temporary bypass, forced signal or changed timer before testing. Never infer a safe setting from an unrelated unit.

    2. Prove pre-start permissives

    Check emergency-stop reset, access-door status, combustion-air availability, fuel pressure within the approved operating window, damper position and instrument health. Record tag status and test method. A permissive that is merely “green” on the HMI still needs field confirmation when practical.

    3. Verify purge and air proving

    Confirm the purge command, damper travel, airflow switch or transmitter response, and the timer’s start and completion events. Capture timestamps or trend screenshots. If airflow cannot be proven, the ignition step must remain unavailable.

    4. Observe ignition and flame proving

    Record igniter energization, pilot or main-fuel valve commands, flame-signal appearance and the permitted proving interval. Keep fuel-train leak checks and local EHS controls inside the test boundary. Do not defeat a trip to make a sequence pass.

    5. Test trip and abort paths

    With the approved test method, simulate loss of air proof, loss of flame, low fuel pressure and emergency stop. Verify that fuel valves close, alarms identify the initiating cause and the sequence returns to a defined safe state. Document reset requirements before another start attempt.

    Evidence table

    Sequence gateEvidence to retainRelease question
    PermissivesTag list, field check, PLC revisionAre all required inputs valid?
    PurgeStart/end timestamps, airflow trendWas the chamber purged under the approved logic?
    IgnitionIgniter and valve command recordDid fuel admission follow the approved order?
    Flame provingSignal trace and timeoutWas flame proven within the allowed interval?
    TripsSimulation result, valve closure, alarmDoes each fault remove fuel and latch correctly?

    Common mistakes

    Typical gaps include testing only from the HMI, omitting a field device check, changing timers without revision control, and accepting an alarm without proving valve closure. Separate functional-test evidence from final operating release so unresolved deviations remain visible.

    Technician checking RTO burner ignition and airflow interlock components

    FAQ

    Is a flame signal alone enough to release the burner?

    No. The signal must be correlated with purge completion, valve order, proving time and trip behavior.

    Can operators bypass a permissive during commissioning?

    Only under a documented, authorized test procedure with compensating controls; bypasses must be removed and verified before service.

    What should the handover package contain?

    Include the approved sequence, revision identifiers, test sheets, timestamps or trends, trip results, deviations and named approvers.

    CTA

    Preparing an RTO restart? Share your cause-and-effect matrix and sequence test sheet with SERNO for an evidence-focused review of burner safety and maintainability.

  • RTO Burner Refractory Inspection: Evidence to Collect Before Restart

    RTO Burner Refractory Inspection: Evidence to Collect Before Restart

    RTO Burner Refractory Inspection: Evidence to Collect Before Restart

    Refractory damage can hide behind a clean-looking burner cabinet. Cracks, displaced tiles and open joints change heat transfer, create local hot spots and may let hot gas bypass the intended flow path. Before restarting an industrial regenerative thermal oxidizer (RTO), the plant team should define what is inspected, what is photographed and who releases the equipment.

    Engineer inspecting refractory lining around an industrial RTO burner chamber

    Why the refractory boundary matters

    The lining protects the steel shell and stabilizes the combustion zone. Inspection should connect physical condition to operating evidence, without assuming that a single temperature reading proves integrity. Record the train, chamber, burner position, access date and operating case for every observation.

    1. Build a chamber-by-chamber map

    Mark burner tile, hearth, sidewall, roof, expansion joints, access doors and thermocouple penetrations on a sketch. Use the same identifiers in photographs and the maintenance work order. This prevents a repair quote from hiding an uninspected corner.

    2. Inspect tile, lining and anchors

    Look for open cracks, spalling, bulging, missing pieces, exposed anchors, powdering and evidence of flame impingement. Do not probe hot refractory or enter a chamber without the site’s isolation, cool-down and confined-space controls. Distinguish surface crazing from a through-joint or displaced section.

    3. Check interfaces and bypass paths

    Inspect burner-to-tile gaps, door seals, expansion joints, crossover areas and transitions to ceramic media. A bypass path can be mechanical, thermal or both. Record gap location and approximate dimensions using an agreed method; do not invent tolerance values when the OEM drawing is unavailable.

    4. Correlate with operating evidence

    Compare the inspection map with chamber temperature trends, burner flame observations, pressure readings and any alarm history. Correlation is a screening tool, not a diagnosis. A qualified engineer should decide whether evidence supports patching, tile replacement, anchor repair or a broader outage scope.

    5. Define a restart release gate

    The release package should include before/after photos, repaired-area identity, materials and batch records when supplied, cure/dry-out instructions, door and joint checks, and sign-off by the responsible operations and maintenance roles. Keep open deviations visible rather than burying them in a general “good condition” statement.

    Inspection evidence checklist

    Evidence rowMinimum recordOwner
    Location mapChamber, burner and elevationMaintenance
    ConditionPhoto plus crack/spall/interface descriptionInspection
    Safety boundaryIsolation, cool-down and access authorizationOperations/EHS
    Repair scopeArea, method, material and cure requirementContractor/OEM
    ReleaseOutstanding deviations and named approverPlant owner

    Common scope mistakes

    Treating burner refractory as a burner-only issue, accepting undated photos, omitting expansion joints, and restarting before cure or dry-out requirements are confirmed can all create avoidable risk. Procurement should ask bidders to price inspection, access, repair, cure support and close-out evidence as separate lines.

    Close inspection view of RTO burner tile and refractory expansion joint

    FAQ

    How often should RTO burner refractory be inspected?

    Use the site maintenance strategy, alarm history and outage plan. Frequency is equipment- and process-specific; the inspection record should explain the trigger.

    Can temperature trends replace a physical inspection?

    No. Trends can identify where to look, but they cannot prove that lining, anchors or joints are intact.

    What should a repair quotation include?

    It should identify access method, chamber locations, removal and installation scope, materials, cure/dry-out support, exclusions and evidence delivered at close-out.

    CTA

    Planning an RTO outage? Share your chamber map, inspection photos and restart constraints with SERNO for a scope review focused on evidence, interfaces and maintainability.

  • RTO Flame Scanner Verification: Prove Burner Safety Signals Before Restart

    RTO Flame Scanner Verification: Prove Burner Safety Signals Before Restart

    RTO Flame Scanner Verification: Prove Burner Safety Signals Before Restart

    An RTO can show normal temperature trends while its flame-detection boundary is misaligned, dirty or incorrectly wired. Before a planned restart, verify the flame scanner as a safety instrument—not as a value to be tuned until the burner “looks right.” This guide separates observable evidence from assumptions so owners can release the burner safely.

    Engineer verifying combustion-air and fuel evidence beside an industrial RTO burner cabinet

    1. Define the flame-detection boundary

    Record burner tag, scanner model, sighting port, flame amplifier and the safety PLC input. Confirm which cabinet, cable and terminal numbers belong to the burner. A marked-up loop drawing and photographs prevent responsibility gaps between burner, controls and RTO suppliers.

    2. Inspect sighting hardware and environment

    With the burner isolated and cool, inspect the sight glass, purge-air tube, mounting bracket and scanner insertion depth. Look for soot, cracked glass, loose glands, vibration marks and hot surfaces that can distort the signal. Confirm purge air is clean, dry and routed as designed; never defeat a purge to obtain a stronger reading.

    3. Prove wiring and signal health

    Compare terminal numbers with the approved schematic. Check shield termination, polarity, 24 VDC supply, fuse status and cable segregation from ignition wiring. Capture scanner status, flame-present input, fault output and any analog strength value at the cabinet. A healthy signal must remain attributable to the correct burner and input.

    4. Test permissives and trip response

    Use the approved commissioning procedure to simulate loss of flame, where permitted. Verify that the safety logic removes fuel, records the correct alarm and requires the intended reset. Check purge-complete, damper position, combustion-air proof and low-fuel-pressure permissives. Do not bypass a trip for production; document test method, witness and restoration.

    5. Release criteria and evidence pack

    CheckEvidence to retainRelease question
    Sighting pathPhoto, cleanliness noteCan the scanner see the intended flame only?
    Purge airPressure/flow indication and sourceIs the lens protected during operation?
    WiringMarked loop and terminal photoDoes the signal land on the correct safety input?
    Flame loss testTimestamped alarm/trip recordDoes fuel shut off without unsafe delay?
    Restart permissivesPLC sequence or checklistAre all gates restored after testing?

    6. Common failure patterns

    Intermittent flame signals often trace to a dirty sight glass, loose bracket, poor purge air or shield noise—not immediately to burner instability. A permanently “flame present” input can indicate a shorted circuit or bypass. Treat each as a safety defect until the physical and logic boundaries are proven.

    7. Coordinate the restart handover

    The handover should name the person who restored each bypass, the exact alarm tested, fuel-valve status, purge status and first-watch readings. Keep the signed checklist with the RTO maintenance record so a later fault can be correlated to a known baseline.

    Inspection of RTO combustion-air damper, filter and burner-register evidence

    FAQ

    How often should an RTO flame scanner be checked?

    Follow the burner OEM and site safety-management schedule; inspect after maintenance, refractory work, repeated trips or any sighting-path disturbance.

    Can operators clean the scanner while online?

    Only if the equipment and site procedure explicitly allow it. Most cleaning requires isolation and verification of the purge and fuel boundary.

    Is a flame-strength number alone enough?

    No. It must agree with physical sighting, correct wiring, permissives and a documented loss-of-flame trip test.

    Professional CTA

    Planning an RTO restart or burner service? Contact SERNO to review the flame-scanner boundary, safety I/O and evidence pack before fuel is reintroduced.

  • RTO Burner Airflow Ratio Verification: Separate Combustion-Air Drift from VOC Load Changes

    RTO Burner Airflow Ratio Verification: Separate Combustion-Air Drift from VOC Load Changes

    RTO Burner Airflow Ratio Verification: Separate Combustion-Air Drift from VOC Load Changes

    When an RTO shows a different chamber temperature, oxygen reading, fuel signal, or pressure trend, plant teams often start with the process exhaust. That can miss a simpler cause: combustion-air flow or damper position has drifted. The correct diagnostic question is not “What is the burner setpoint?” but “What air-to-fuel condition existed at the same verified process load?”

    Engineer verifying combustion-air and fuel evidence beside an industrial RTO burner cabinet

    This guide lays out a measurement boundary for checking burner airflow ratio without inventing a universal ratio. Final limits must come from the approved burner package, OEM instructions, fuel train design, combustion safeguards, and site procedures.

    1. Define the comparison case

    Select a stable operating window and document which chambers, burners, bypasses, and exhaust sources were active. Record production state, solvent or coating family where relevant, source capture status, inlet VOC measurement if available, chamber temperature, oxygen, fuel command, and fan operating point. A reduced-shift case cannot be compared directly with a full-production case.

    2. Map the combustion-air path

    Identify the combustion-air fan, filters, inlet louver, manual and control dampers, flexible connections, burner registers, and any dilution or purge-air tie-ins. Record measurement locations and whether the value is a calibrated flow, a pressure proxy, or only a command signal. A damper percentage is not proof of delivered airflow.

    3. Verify instruments before interpreting trends

    Check calibration status, impulse lines, transmitter zero, temperature and pressure compensation, and the time alignment of historian tags. Confirm that airflow units and reference conditions are consistent. If a flow element is outside its validated range, label the reading as indicative rather than quantitative.

    4. Build the ratio evidence table

    Evidence rowRecordWhy it matters
    Combustion-air flowInstrument, location, units, reference basisConfirms delivered air rather than command position
    Fuel flow or valve positionMeter/tag and stable time windowDefines the paired fuel condition
    Burner oxygen or flue-gas oxygenLocation, temperature basis, analyzer statusShows the combustion response, not just the input
    Air and fuel pressureUpstream/downstream pointsReveals restriction or regulator drift
    Damper/register positionFeedback plus physical inspection statusDetects linkage or feedback mismatch
    Process/VOC stateActive sources and measured trendPrevents combustion drift being blamed on load

    Compare rows at the same timestamp and under the same approved firing mode. Do not calculate a ratio from unrelated historian averages.

    5. Separate air-path faults from VOC-load changes

    If fuel and combustion-air signals move together while process conditions remain stable, investigate control logic, regulator behavior, and burner sequencing. If combustion-air pressure changes while the command remains constant, inspect filters, louvers, fan condition, and dampers. If oxygen changes with stable air and fuel evidence but VOC loading changes, review the oxidizer heat-release balance and sampling boundary instead of immediately retuning the burner.

    6. Use safe adjustment gates

    Any adjustment should have a written setpoint range, interlock status, flame-safeguard readiness, responsible person, rollback condition, and post-change observation window. Never bypass purge, flame failure, high-temperature, or pressure protections to obtain a “clean” test. Record the pre-change state so the result remains attributable.

    7. Specify the procurement and service scope

    When requesting support, define whether the supplier must measure airflow, verify burner registers, inspect filters and dampers, validate analyzer signals, or retune control parameters. Ask for raw readings, instrument references, operating cases, and acceptance criteria—not only a final ratio number.

    Inspection of RTO combustion-air damper, filter and burner-register evidence

    FAQ

    Is there one correct RTO burner airflow ratio?

    No. The acceptable relationship depends on burner design, fuel, firing mode, excess-air requirements, safeguards, and the OEM-approved operating envelope.

    Can oxygen alone prove the burner ratio?

    No. Oxygen is a response indicator affected by leakage, dilution, sampling location, temperature, and process conditions. Pair it with airflow, fuel, pressure, and operating-state evidence.

    Should a higher VOC reading trigger more combustion air?

    Not automatically. Confirm the measurement boundary, heat-release trend, chamber temperature, and approved control philosophy before changing combustion settings.

    Practical CTA

    SERNO can help teams define an RTO combustion-air verification scope, measurement points, and evidence checklist for a retrofit, commissioning review, or troubleshooting visit. Share the burner type, fuel, available tags, and operating cases for a technically bounded review.

  • RTO Fan VFD Operating Point: Verify Airflow Before Changing Frequency

    RTO Fan VFD Operating Point: Verify Airflow Before Changing Frequency

    RTO Fan VFD Operating Point: Verify Airflow Before Changing Frequency

    A variable-frequency drive makes an RTO exhaust fan adjustable, but the displayed frequency is not an airflow measurement. Two systems running at the same hertz can deliver different flow because dampers, filters, duct resistance, process openings, gas density, fan condition, and production simultaneity are different.

    Engineer reviewing an RTO exhaust fan VFD operating point beside the connected duct and treatment system

    Changing frequency without recording the operating context can move a problem rather than solve it. Too little extraction may weaken source capture. Too much can increase energy use, entrain unwanted air, disturb ovens or booths, raise duct velocity, and shift the oxidizer load. This guide explains the evidence an industrial team should assemble before accepting or changing an RTO fan operating point. Final limits must come from the approved fan curve, motor data, process design, control philosophy, and site safety procedures.

    1. Define the Required Duty Before Reading the VFD

    Start with the service the fan must provide: which exhaust sources are open, which production lines can run together, required capture conditions, design flow at stated reference conditions, and the pressure needed to overcome the connected system resistance.

    Record whether the fan is on the clean or dirty side of the treatment train and whether the control target is duct pressure, hood pressure, airflow, oven balance, or another verified process variable. A frequency setpoint is only a means of reaching the required duty; it is not the duty itself.

    2. Record the Complete Operating Context

    An operating-point record should identify the production state at the same time as the measurements. Include active sources, product or coating family where relevant, open doors or bypasses, filter condition, damper positions, ambient conditions, exhaust temperature, and any maintenance or process change.

    Avoid comparing a full-production reading with a reduced-shift reading as though the duct network were unchanged. Mark temporary hoses, isolated branches, added extraction points, and manual damper adjustments. These details often explain why the same frequency produces a different pressure or flow.

    3. Measure Airflow and Pressure at Defined Locations

    Use suitable, maintained instruments and documented measurement locations. A single velocity reading near an elbow, damper, transition, or fan connection may not represent the average duct velocity. Where a traverse is required, use the applicable site or engineering method and record the duct dimensions, temperature, pressure, and reference basis.

    Pressure readings also need context. State whether each value is static, velocity, or total pressure and identify the upstream and downstream locations. Trend filter differential pressure separately from overall system resistance. Never infer capture performance solely from fan inlet suction if branch conditions are unknown.

    Engineer recording VFD frequency, pressure, and operating context for an RTO exhaust fan

    4. Use the Fan Curve and System Curve Together

    The fan operating point is where the fan capability and system resistance meet. Review the approved fan curve for the actual wheel, rotation, speed range, gas density, and configuration. Confirm that the selected point remains inside the documented operating envelope and does not overload the motor.

    Fan affinity relationships can support preliminary reasoning for the same system near similar conditions: flow changes approximately with speed, pressure with speed squared, and power with speed cubed. They are not a substitute for measurements when dampers move, filters load, branches change, gas properties vary, or the fan is operating outside the assumptions.

    5. Check Motor, VFD, and Mechanical Evidence

    Record frequency, commanded speed, actual speed if available, motor current, power, voltage, drive alarms, bearing condition, and vibration together. Compare them with approved nameplate and supplier limits without inventing a universal acceptance value.

    A low current does not prove adequate airflow, and a high current does not identify the cause by itself. Unexpected load can come from excessive flow, density changes, mechanical condition, control settings, or an incorrect fan configuration. Confirm minimum-speed, acceleration, cooling, resonance-avoidance, and interlock requirements from the equipment documentation.

    6. Confirm Capture and Process Stability

    The correct fan point must work at the sources. Observe or measure the approved capture indicators at hoods, booths, ovens, enclosures, and room boundaries. Check for odor escape, visible migration where a safe approved method exists, door interference, excessive inward draft, process temperature disturbance, or unstable burner and pressure-control behavior.

    Do not increase fan speed as the first response to every capture complaint. A closed damper, disconnected branch, blocked filter, damaged hood, open access door, poor make-up air, or changed production layout may be the real cause.

    7. Build an Operating-Point Evidence Table

    Evidence groupRecord togetherDecision question
    Production stateactive lines, source simultaneity, doors and bypassesDoes the test represent the intended operating case?
    Air networkdamper positions, filter DP, branch status, make-up airIs the network configuration known and repeatable?
    Flow and pressuremethod, location, reference conditions, measured valuesIs required capture achieved with traceable measurements?
    Fan and drivefrequency, speed, current, power, alarmsIs the duty inside approved fan, motor, and VFD limits?
    Mechanical conditionvibration, bearings, noise, flexible connectionIs mechanical behavior stable at this point?
    Treatment processinlet state, relevant temperatures and pressureDoes the RTO remain stable as airflow changes?
    Release recorddate, instruments, personnel, deviations, approvalCan the operating point be reproduced and audited?

    8. Control Setpoint Changes and Revalidate

    Treat a permanent frequency change as a controlled change. Record the previous setpoint, reason, authorized range, affected recipes or modes, test sequence, results, and rollback condition. Protect critical parameters with the plant’s access-control and change-management process.

    After adjustment, repeat the relevant capture, airflow, pressure, motor-load, vibration, and treatment-process checks at the defined production cases. One successful moment is not enough if the plant has multiple operating modes. Establish a baseline that future teams can compare with the same measurement locations and operating context.

    FAQ

    Does 50 or 60 Hz mean the fan is delivering design airflow?

    No. Frequency indicates the drive command, not verified flow. Actual duty depends on fan configuration, system resistance, gas conditions, damper positions, filter loading, and the connected sources.

    Can fan frequency be increased to fix poor hood capture?

    Only after checking the cause and approved operating limits. Poor capture may come from hood geometry, branch isolation, filter blockage, make-up-air imbalance, open doors, or a changed process rather than insufficient fan speed.

    Which readings should be stored with a VFD setpoint?

    Store the production state, branch and damper configuration, airflow and pressure measurement details, filter differential pressure, temperature, fan speed or frequency, motor load, vibration, capture observations, and any deviations.

    Should affinity laws be used to choose the new setpoint?

    They can support an engineering estimate when their assumptions are valid, but field measurements and the approved fan/system data are still required. Network changes and variable gas conditions can invalidate a simple speed ratio.

    Professional CTA

    If you are reviewing an RTO fan setpoint, retrofit, or proposal, SERNO can help structure the engineering questions around exhaust sources, airflow cases, pressure loss, fan selection, VFD control, capture evidence, and treatment-system stability. Share verified process data and available drawings for a technical discussion; final settings and limits must be confirmed for the specific installation.

  • RTO Fan Flexible Connection Inspection: Check Duct Loads Before Restart

    RTO Fan Flexible Connection Inspection: Check Duct Loads Before Restart

    RTO Fan Flexible Connection Inspection: Check Duct Loads Before Restart

    An induced-draft fan is often connected to an RTO duct by a fabric or metallic flexible element. Its purpose is limited: accommodate specified movement, isolate part of the vibration transmission, and tolerate normal thermal growth. It is not a structural support, an alignment correction, or a substitute for properly restrained ductwork.

    Technician inspecting an RTO fan flexible connector, flange, and adjoining duct supports before restart

    When the connector wrinkles unevenly, pulls sideways, tears near a flange, or repeatedly loosens bolts, replacing the connector alone may only reset the failure clock. The inspection should determine what load the adjoining duct and supports are imposing on the fan connection. This guide provides a practical shutdown review for industrial buyers, maintenance teams, and engineers. Actual acceptance limits must come from the fan, connector, duct, and support documentation for the installed system.

    1. Define the Connector’s Intended Movement

    Start with the design basis rather than the damaged appearance. Identify the connector type, material, temperature rating, flow direction, installed face-to-face dimension, and permitted axial, lateral, and angular movement. Confirm whether an internal liner, flow sleeve, insulation blanket, or external restraint is part of the assembly.

    Compare the approved drawing with the installed arrangement. A connector fitted shorter, longer, or more offset than its intended neutral geometry may already be consuming its movement allowance while the system is cold. Photograph the four sides with a scale before loosening anything.

    2. Inspect the Fabric, Flanges, and Fasteners

    With the exhaust train isolated, locked out, cooled, and verified safe under the plant procedure, inspect the full circumference. Look for:

    • abrasion, pinholes, delamination, hardening, blistering, or heat discoloration;
    • folds concentrated on one side and tension on the opposite side;
    • damage close to bolt bars or flange corners;
    • loose, missing, mismatched, or bottomed-out fasteners;
    • gasket extrusion, uneven clamp pressure, and signs of gas leakage;
    • contact between the flexible element and an internal liner or nearby steelwork.

    Do not infer material fitness from appearance alone. If the process has changed, check the actual temperature, solvent composition, moisture, mist, and cleaning exposure against the connector supplier’s documented limits.

    3. Check Cold Alignment Before Disconnecting the Joint

    Record the fan inlet or outlet flange position relative to the adjoining duct flange. Useful evidence includes gap measurements at several clock positions, centerline offset, flange parallelism, connector face-to-face dimension, and photographs from fixed reference points.

    If the joint is disconnected, the duct should not jump, drop, rotate, or spring sideways. Unexpected movement indicates stored load or inadequate support. Plan temporary support before releasing bolts; a flexible connector must never become the item holding the duct in place.

    RTO duct and fan interface inspected for alignment, support condition, and imposed duct load

    4. Review Duct Supports, Guides, and Anchors

    Follow the load path away from the connector. Inspect support shoes, hangers, springs, guides, anchors, structural steel, and base fasteners. Search for loose anchors, cracked grout, bent brackets, polished rub marks, elongated holes, missing slide plates, seized guides, or insulation preventing intended movement.

    The question is not simply whether supports exist. Ask whether each support still performs its assigned function when the duct is cold, hot, under fan suction, and exposed to wind or maintenance loads. Field modifications, added silencers, dampers, access platforms, or heavier insulation can change the original load path.

    5. Separate Thermal Movement from Installation Misalignment

    Thermal growth should move through the intended guides and expansion features. Installation misalignment is a cold geometric error. The two can produce similar connector distortion but require different corrections.

    Use available cold and operating measurements to compare positions. If distortion appears only when hot, review thermal movement, guides, and anchors. If the connector is already offset when cold, review erection alignment and support elevation. If movement follows fan speed or damper position, investigate aerodynamic loading and pressure pulsation as well as mechanical support.

    6. Build a Restart-Release Evidence Table

    Inspection itemEvidence to recordRelease question
    Connector identitytype, material, drawing/reference, installed dimensionIs it the approved part for temperature and process exposure?
    Flexible elementfour-side photos, wear and leakage observationsIs it intact and free from damaging contact or pre-tension?
    Flanges and boltsgap, parallelism, bolt condition, clamp patternAre flanges aligned and uniformly clamped?
    Duct supportsupport ID, condition, elevation, free/sliding statusDoes the duct remain independently supported?
    Guides and anchorsposition, looseness, rub marks, unauthorized changesCan thermal growth follow the intended path?
    Fan base interfacebase bolts, grout, soft-foot or movement observationsIs the fan position stable without duct forcing?
    Cold run readinessguards, tools cleared, temporary supports removedIs the train safe for a controlled first run?
    First-run baselinevibration, noise, pressure, temperature, connector movementDoes behavior remain within approved limits and baseline expectations?

    7. Verify the Interface During a Controlled Restart

    After corrective work, complete the plant’s pre-start safety review. Observe the connector from a safe position during the controlled first run. Watch for rapid inflation or collapse, flutter, rubbing, abnormal movement, leakage, new noise, and changes as dampers or fan speed move through the planned operating range.

    Record fan vibration, relevant pressure readings, bearing condition, connector position, and operating state together. A single measurement without airflow, temperature, damper position, and production context is difficult to compare later. Stop and investigate if the connector or duct moves in a way that was not anticipated by the approved design.

    8. Clarify Responsibility Before the Next Outage

    Define who owns connector specification, spare supply, duct-support inspection, fan alignment, insulation removal and reinstatement, lifting and temporary support, first-run monitoring, and final release. These boundaries often span the fan supplier, duct contractor, RTO integrator, maintenance team, and plant engineering.

    For procurement or retrofit work, request interface drawings and allowable connection loads rather than accepting “flexible joint included” as a complete scope description. The commercial boundary should state who verifies that the installed duct does not impose unacceptable forces or moments on the fan.

    FAQ

    Can a flexible connector correct duct misalignment?

    It may physically accommodate limited movement within its approved range, but it should not be used to conceal poor cold alignment or carry structural duct load. Correct the load path and geometry first.

    Should the connector be tight when the system is cold?

    Not by assumption. The required neutral geometry depends on the connector design and expected thermal movement. Compare the installed dimension and offset with approved documentation.

    Why does a replacement connector fail again?

    Repeated failure can result from unresolved misalignment, unsupported duct weight, seized guides, excessive movement, heat or chemical exposure, abrasion, pressure pulsation, or incorrect installation. Preserve evidence before removing the failed part.

    What should be measured after restart?

    At minimum, record the operating state, relevant pressures and temperatures, fan vibration, abnormal noise, leakage, and visible connector movement. Use the equipment documentation and plant procedures to define limits.

    Professional CTA

    If you are comparing a new RTO package or reviewing a fan-duct retrofit, SERNO can help organize the interface questions: exhaust conditions, fan operating range, connector material, support arrangement, thermal movement, access, spares, and restart evidence. Share drawings and verified process data for an engineering discussion; final limits must be confirmed for the specific installation.

  • RTO Fan Vibration Diagnosis: Mechanical vs Process Causes

    RTO Fan Vibration Diagnosis: Mechanical vs Process Causes

    RTO Fan Vibration Diagnosis: Mechanical vs Process Causes

    An induced-draft fan can vibrate because of an unbalanced wheel, bearing damage, misalignment, looseness, resonance, or foundation problems. The same symptom can also appear when deposits build unevenly, dampers create unstable inlet flow, duct pressure changes, temperature shifts the structure, or the fan operates far from its intended duty point.

    Industrial induced-draft fan and ductwork during an RTO vibration inspection

    Replacing bearings before separating these causes can create cost without removing the trigger. A useful investigation preserves the operating context, compares repeatable measurements, and links each proposed action to evidence.

    1. Protect people and equipment before collecting data

    Follow the site procedure, fan and RTO OEM instructions, guarding requirements, lockout rules, hot-surface controls, and gas-hazard precautions. Do not approach rotating equipment, open inspection doors, or change dampers solely to create a test condition without an approved plan.

    Use the applicable OEM or site alarm and shutdown criteria. A universal vibration limit is not appropriate because machine size, speed, bearing arrangement, measurement location, sensor type, and acceptance standard differ.

    2. Record the exact operating condition

    Vibration amplitude alone is weak evidence. Record fan speed, motor current, damper or VFD command, inlet and outlet pressure, gas temperature, production sources online, RTO mode, recent washdown or shutdown, and the time since startup. Note whether the reading is steady, cyclic, or tied to a process event.

    Compare like with like. A measurement at cold startup should not be treated as directly equivalent to one after thermal stabilization.

    3. Establish a repeatable vibration map

    Collect readings at consistent bearing locations and directions using the same instrument settings and units. Preserve overall values and, where competent resources are available, spectral and phase information. Mark sensor positions so follow-up measurements can be repeated.

    Trend changes against a known acceptable baseline. If no baseline exists, document the current condition carefully rather than inventing one.

    4. Separate mechanical fault patterns from process-side clues

    ObservationPossible mechanical causesPossible process-side causesEvidence to collect
    Speed-related vibrationWheel imbalance, shaft issue, coupling conditionUneven deposit buildup, product carryoverSpectrum, wheel inspection, process history
    Higher vibration after warm-upThermal growth, alignment shift, loosenessGas-temperature or density change, duct load transferCold/hot alignment evidence, temperatures, supports
    Cyclic or unstable vibrationLooseness, resonanceInlet swirl, damper hunting, unstable system pressureDamper/VFD trend, pressure trend, phase evidence
    Sudden step changeComponent damage, lost balance weight, bearing eventDeposit release, process upset, liquid or particulate carryoverEvent timeline, inspection, upstream records
    Vibration with rising motor loadRubbing, bearing conditionIncreased system resistance, fouling, changed airflowCurrent, pressure, speed, filter/duct condition

    No single row proves a cause. Use it to plan discrimination tests and inspections.

    5. Inspect the airflow path, not only the fan

    Review inlet geometry, flexible connections, dampers, turning vanes, duct supports, drains, filters, access doors, and upstream carryover controls. Check whether recent production changes altered airflow, solvent loading, particulate loading, or moisture. An asymmetric inlet condition or fouled wheel can mimic a purely mechanical defect.

    Document deposits before cleaning. Their location and composition may explain why balance changed and what upstream corrective work is needed.

    6. Review bearings, alignment, structure, and resonance

    With the equipment safely isolated, inspect fasteners, baseplate and grout condition, bearing mounting, lubrication evidence, coupling condition, guards, soft foot, shaft alignment, and signs of rubbing or heat. Review whether connected ductwork is imposing load on the fan casing.

    If resonance is suspected, use qualified vibration analysis rather than trial-and-error structural changes. A reinforcement or speed change can move, not necessarily solve, the response.

    7. Define an evidence-based corrective scope

    The work scope should state the measured condition, operating case, probable cause and uncertainty, required inspections, cleaning boundary, balance or alignment method, bearing and coupling requirements, duct/support interfaces, hold points, acceptance criteria, and records to return.

    Separate immediate protection actions from permanent corrective work. If deposits caused imbalance, balancing the wheel without controlling the carryover leaves the recurrence mechanism in place.

    8. Verify the repair under comparable conditions

    After work, confirm guards, fasteners, lubrication, alignment records, damper lineup, instrument restoration, and removal of temporary items. Conduct a controlled startup under the approved procedure. Trend vibration, speed, motor current, pressure, and temperature through cold and thermally stable conditions where applicable.

    Acceptance should use the agreed OEM/site criteria and a comparable operating point. Keep the as-left map as the new reference only when the operating condition is clearly recorded.

    Buyer checklist

    • Fan tag, arrangement, speed range, motor data, and latest drawings
    • Measurement locations, units, settings, spectra, phase, and timestamps
    • Operating mode, airflow/pressure, temperature, motor current, and production state
    • Wheel, bearing, coupling, base, flexible-connection, and duct-support inspection evidence
    • Deposit or carryover evidence and upstream process history
    • OEM/site limits and shutdown logic—not assumed generic limits
    • Corrective scope, hold points, balancing/alignment records, and restart results

    FAQ

    Does high vibration always mean the bearings are failing?

    No. Bearing damage is one possibility, but imbalance, looseness, misalignment, resonance, rubbing, fouling, inlet-flow distortion, and changing operating conditions can produce similar symptoms.

    Can the fan simply be balanced in place?

    Field balancing may be appropriate when performed by qualified personnel under an approved method, but the wheel condition, deposits, structural integrity, operating point, and upstream recurrence mechanism should be reviewed first.

    Why does vibration change after the RTO warms up?

    Thermal growth can affect alignment, clearances, supports, and connected duct loads. Gas temperature and density can also shift fan duty. Comparable cold and stable-hot evidence helps separate these effects.

    What information should be sent with an RFQ?

    Provide the fan identity, drawings, operating cases, vibration data and locations, speed/current/pressure/temperature trends, inspection photos, event history, required acceptance criteria, and the expected reporting deliverables.

    Professional CTA

    Planning an RTO fan investigation or repair RFQ? Send SERNO the fan arrangement, operating data, vibration records, duct layout, inspection evidence, and site acceptance requirements. We can help structure the technical review and identify the information needed before equipment scope is finalized.

    Internal link suggestions

    • Link to the existing RTO pressure-drop and fan-sizing guide from the airflow-path section.
    • Link to the expansion-joint inspection article from the duct-load discussion.
    • Link to the filter stock-planning article from the fouling and system-resistance discussion.